In the world of industrial automation, the Food Grade Solenoid Valve stands as a cornerstone of precision and reliability. This article delves into the intricacies of these valves, their applications, and the reasons why they are indispensable in the food and beverage industry.
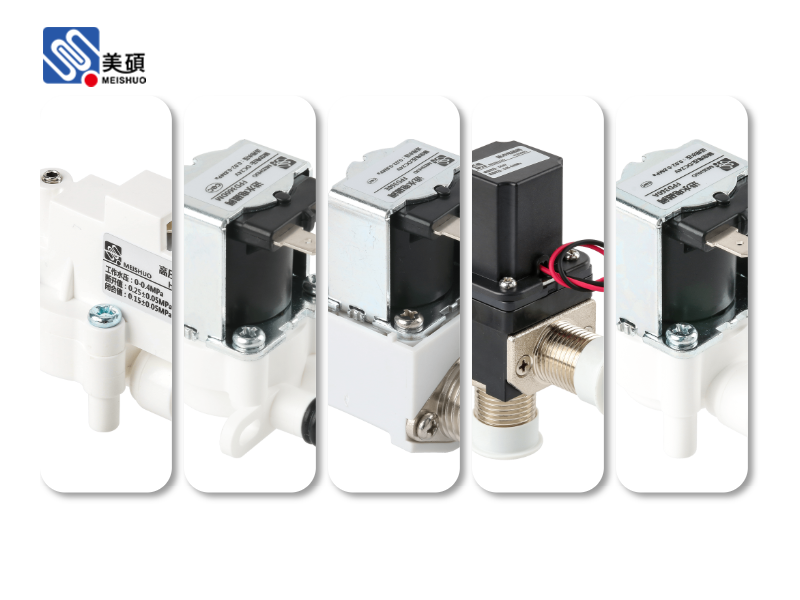
The Basics of Food Grade Solenoid Valves A Food Grade Solenoid Valve is a type of electromechanical device that uses an electromagnetic coil to open or close a valve. These valves are specifically designed to handle food-grade applications, where hygiene and safety are paramount. The materials used in their construction are non-toxic and resistant to corrosion, ensuring that they do not contaminate the food or beverage products they are used to control.
Applications in the Food and Beverage Industry The food and beverage industry is highly regulated, and the use of Food Grade Solenoid Valves is essential for maintaining compliance with these standards. These valves are used in a variety of applications, including:
1. **Pumping Systems**: They control the flow of liquids in pumping systems, ensuring that the correct amount of product is delivered without contamination. 2. **Filling Machines**: In bottling and packaging operations, Food Grade Solenoid Valves are used to control the flow of liquids into bottles and containers. 3. **Cleaning Systems**: They play a crucial role in cleaning operations, allowing for the precise control of cleaning agents and water. 4. **Process Control**: These valves are used in process control systems to regulate the flow of ingredients and other materials in food processing plants.
Benefits of Using Food Grade Solenoid Valves There are several key benefits to using Food Grade Solenoid Valves in the food and beverage industry:
1. **Hygiene**: The materials used in these valves are non-toxic and resistant to corrosion, making them ideal for food-grade applications. 2. **Reliability**: These valves are designed for heavy-duty use and can withstand harsh conditions, ensuring consistent performance. 3. **Precision**: The precise control offered by these valves is crucial for maintaining the quality of food and beverage products. 4. **Ease of Maintenance**: These valves are designed for easy maintenance, reducing downtime and improving overall efficiency.
Challenges and Solutions Despite their many benefits, Food Grade Solenoid Valves face certain challenges in the food and beverage industry:
1. **Corrosion**: Exposure to aggressive chemicals and high temperatures can lead to corrosion. To combat this, manufacturers use materials like stainless steel and PTFE (Teflon) to ensure longevity. 2. **Temperature Fluctuations**: Extreme temperature changes can affect the performance of these valves. To address this, thermal relief valves are often used to protect the valve from temperature extremes.
Future Trends The future of Food Grade Solenoid Valves looks promising, with several trends emerging:
1. **Smart Valves**: The integration of sensors and smart technology into Food Grade Solenoid Valves is expected to increase, providing real-time data and predictive maintenance capabilities. 2. **Sustainability**: As the world becomes more environmentally conscious, there is a growing demand for valves made from sustainable materials.
Conclusion Food Grade Solenoid Valves are an essential component of the food and beverage industry, providing precision, reliability, and hygiene. As technology continues to advance, these valves are expected to become even more sophisticated, offering even greater benefits to the industry.
 Chat Oline