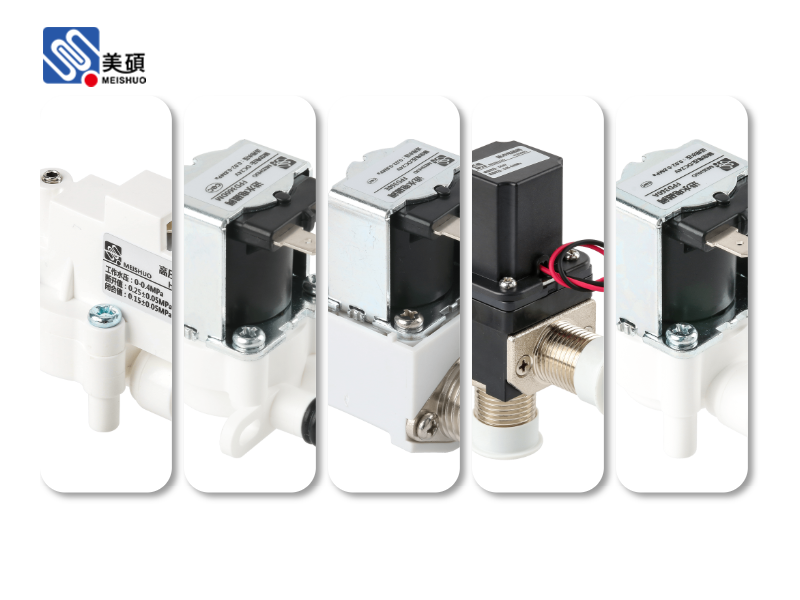
In today's fast-paced industrial environment, the demand for high-quality, reliable components has never been greater. One such component that plays a crucial role in various industries is the solenoid valve. However, not all solenoid valves are created equal. The term 'RoHS Compliant Solenoid Valve' has gained significant importance due to its environmental and health benefits. In this article, we will delve into the significance of RoHS compliance in solenoid valves and how it can maximize efficiency in industrial applications.
**Introduction**
Solenoid valves are electromechanical devices that control the flow of fluids, such as water, air, and oil, in industrial processes. They are widely used in various industries, including automotive, pharmaceutical, food and beverage, and chemical processing. The RoHS directive, also known as the Restriction of Hazardous Substances Directive, is a European Union regulation that restricts the use of certain hazardous substances in electrical and electronic equipment.
**What is RoHS Compliance?**
RoHS compliance refers to the adherence of a product to the RoHS directive. This directive aims to reduce the environmental impact of electrical and electronic equipment by restricting the use of hazardous substances such as lead, cadmium, mercury, hexavalent chromium, polybrominated biphenyls (PBBs), and polybrominated diphenyl ethers (PBDEs).
**Benefits of RoHS Compliant Solenoid Valves**
1. **Environmental Protection**: By using RoHS compliant solenoid valves, industries can minimize their environmental footprint. These valves contain fewer hazardous substances, making them easier to recycle and dispose of at the end of their life cycle.
2. **Health and Safety**: RoHS compliant solenoid valves reduce the risk of exposure to harmful substances, ensuring the safety of workers and consumers. This is particularly important in industries where human contact with hazardous materials is a concern.
3. **Market Access**: Many countries, including the European Union, require RoHS compliance for electrical and electronic products. By using RoHS compliant solenoid valves, manufacturers can ensure their products meet these regulations and gain access to a wider market.
4. **Cost Savings**: Although RoHS compliant solenoid valves may have a higher initial cost compared to non-compliant valves, they can lead to long-term cost savings. These valves have a longer lifespan and lower maintenance requirements, reducing overall operational costs.
**Maximizing Efficiency with RoHS Compliant Solenoid Valves**
1. **Improved Performance**: RoHS compliant solenoid valves are designed to provide optimal performance, ensuring smooth and efficient fluid flow in industrial processes.
2. **Enhanced Reliability**: These valves are built with high-quality materials and advanced manufacturing techniques, resulting in increased reliability and reduced downtime.
3. **Customization**: Many manufacturers offer customizable RoHS compliant solenoid valves, allowing industries to tailor the product to their specific requirements.
4. **Integration**: RoHS compliant solenoid valves can be easily integrated into existing systems, making them a versatile choice for various applications.
**Conclusion**
In conclusion, RoHS compliant solenoid valves offer numerous benefits that can maximize efficiency in industrial applications. By choosing RoHS compliant valves, industries can not only contribute to environmental protection and health and safety but also gain a competitive edge in the global market. As the demand for sustainable and reliable components continues to grow, RoHS compliant solenoid valves will undoubtedly play a crucial role in shaping the future of industrial automation.
 Chat Oline