In the food and beverage industry, ensuring the safety and quality of products is paramount. One critical component that plays a vital role in maintaining these standards is the food grade solenoid valve. This article delves into the importance of food grade solenoid valve certification, its benefits, and the process involved in obtaining it.
**Introduction**
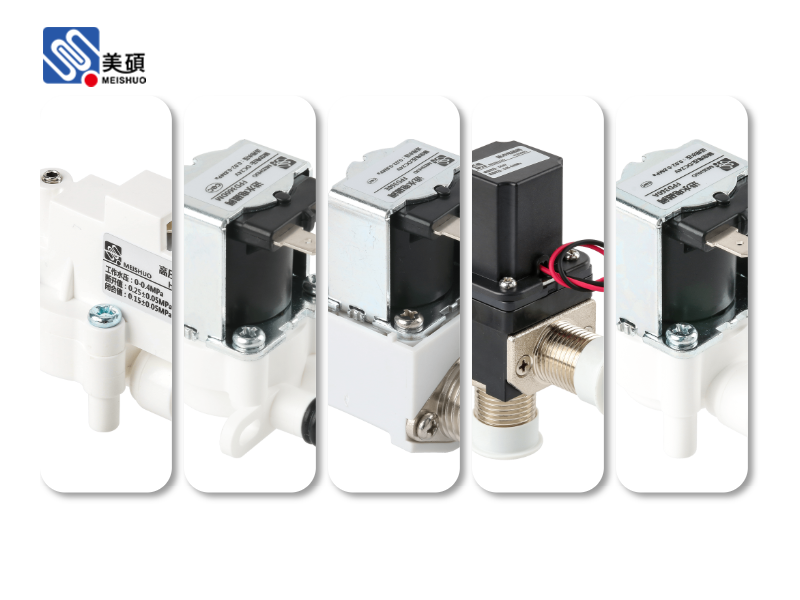
Food grade solenoid valves are specifically designed for use in food processing and packaging applications. These valves are constructed with materials that are safe for contact with food, ensuring that they do not contaminate or degrade the quality of the products. Certification of these valves is essential to validate their compliance with stringent industry standards and regulations.
**The Significance of Food Grade Solenoid Valve Certification**
1. **Compliance with Regulations**: Food grade solenoid valve certification ensures that the valves meet the necessary regulatory requirements set by international and local authorities. This includes adhering to standards such as FDA (Food and Drug Administration), 3A Sanitary Standards, and CE marking.
2. **Enhanced Product Safety**: By using certified food grade solenoid valves, companies can significantly reduce the risk of food contamination. These valves are designed to withstand harsh environments, minimizing the chances of leakage or failure.
3. **Improved Reputation**: Certification serves as a testament to a company's commitment to quality and safety. It can enhance the brand's reputation and build trust among customers and regulatory bodies.
**Benefits of Food Grade Solenoid Valve Certification**
1. **Cost-Effective**: While the certification process may involve some initial investment, it can lead to long-term cost savings. Certified valves require less maintenance and have a longer lifespan, reducing downtime and repair costs.
2. **Increased Efficiency**: Food grade solenoid valves are designed to optimize performance in food processing applications. Certification ensures that these valves operate efficiently, improving overall production processes.
3. **Global Market Access**: Certification allows companies to access international markets that have stringent safety and quality standards. This can open up new business opportunities and expand the customer base.
**The Certification Process**
1. **Material Selection**: The first step in obtaining food grade solenoid valve certification is to ensure that the materials used in their construction are safe for food contact. This includes materials such as stainless steel, polypropylene, and EPDM rubber.
2. **Design and Construction**: The design and construction of the valve must comply with relevant standards. This involves ensuring that the valve is easy to clean, maintain, and sanitize.
3. **Testing and Evaluation**: Certified laboratories conduct rigorous testing to evaluate the performance, safety, and reliability of the food grade solenoid valve. This includes tests for pressure, temperature, flow rate, and material compatibility.
4. **Documentation and Certification**: Once the valve passes all tests, the manufacturer must provide comprehensive documentation to the certifying body. This documentation includes material specifications, design drawings, and test results.
**Conclusion**
Food grade solenoid valve certification is a crucial aspect of ensuring the safety and quality of products in the food and beverage industry. By adhering to stringent standards and regulations, companies can enhance their reputation, improve efficiency, and access new markets. Investing in certified food grade solenoid valves is a wise decision that can lead to long-term benefits for businesses and consumers alike.
 Chat Oline