The food industry is one of the most critical sectors in the global economy, and ensuring the safety and quality of food products is paramount. In this context, the Food Grade Solenoid Valve plays a pivotal role in maintaining the integrity of the food processing environment. This article delves into the significance of Food Grade Solenoid Valves, their functioning, and their impact on the food industry.
**Introduction**
Food Grade Solenoid Valves are specialized devices designed to control the flow of fluids in food processing systems. These valves are crucial in maintaining hygiene, preventing contamination, and ensuring the quality of food products. As the demand for safe and high-quality food continues to rise, the importance of Food Grade Solenoid Valves cannot be overstated.
**Understanding Food Grade Solenoid Valves**
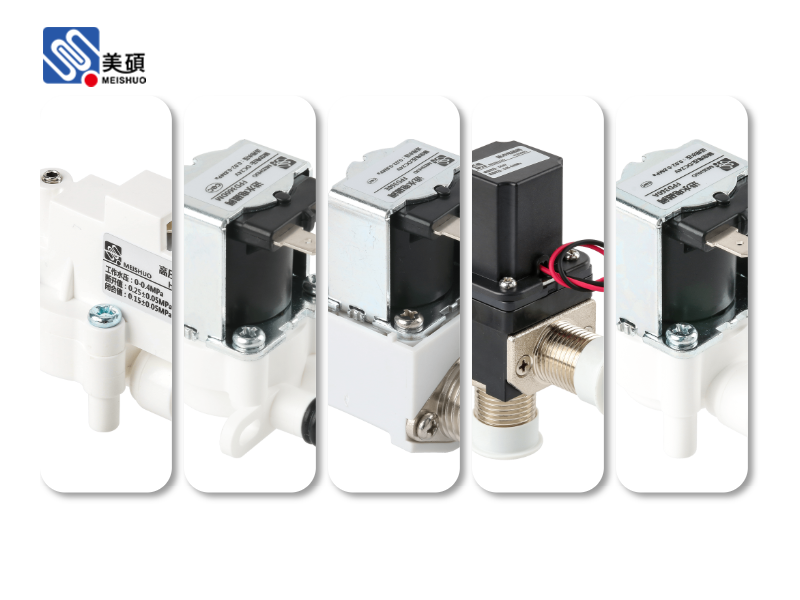
Food Grade Solenoid Valves are specifically engineered to meet the stringent requirements of the food industry. They are made from materials that are non-toxic, corrosion-resistant, and easy to clean. These valves are designed to handle a wide range of fluids, including water, oil, and various food-grade chemicals.
The core component of a Food Grade Solenoid Valve is the solenoid coil, which is responsible for actuating the valve. When an electrical current passes through the coil, it generates a magnetic field that moves the valve's plunger, opening or closing the valve. This mechanism ensures precise control over the flow of fluids, which is essential in food processing.
**Significance in Food Processing**
1. **Hygiene and Sanitation**: One of the primary concerns in the food industry is hygiene and sanitation. Food Grade Solenoid Valves are designed to be easy to clean and maintain, reducing the risk of contamination. The smooth surfaces and tight seals of these valves prevent the accumulation of bacteria and other harmful microorganisms.
2. **Quality Control**: Consistency in the quality of food products is crucial. Food Grade Solenoid Valves ensure precise control over the flow of fluids, which helps in maintaining the desired quality and taste of food products.
3. **Safety**: The food industry is subject to strict safety regulations. Food Grade Solenoid Valves are designed to meet these regulations, ensuring the safety of both consumers and employees.
4. **Efficiency**: These valves are designed to operate efficiently, reducing energy consumption and minimizing downtime. This efficiency translates into cost savings for food processing companies.
**Types of Food Grade Solenoid Valves**
There are several types of Food Grade Solenoid Valves, each designed to handle specific applications in the food industry. Some of the common types include:
1. **Diaphragm Valves**: These valves are ideal for handling aggressive fluids and are commonly used in the dairy and beverage industries.
2. **Ball Valves**: Known for their durability and reliability, ball valves are suitable for high-pressure applications in the food industry.
3. **Pilot Operated Valves**: These valves provide precise control over the flow of fluids and are often used in critical applications.
**Conclusion**
In conclusion, the Food Grade Solenoid Valve is an indispensable component in the food processing industry. Its ability to ensure hygiene, quality, safety, and efficiency makes it a crucial tool for food processing companies. As the demand for safe and high-quality food continues to grow, the role of Food Grade Solenoid Valves will only become more significant.
 Chat Oline