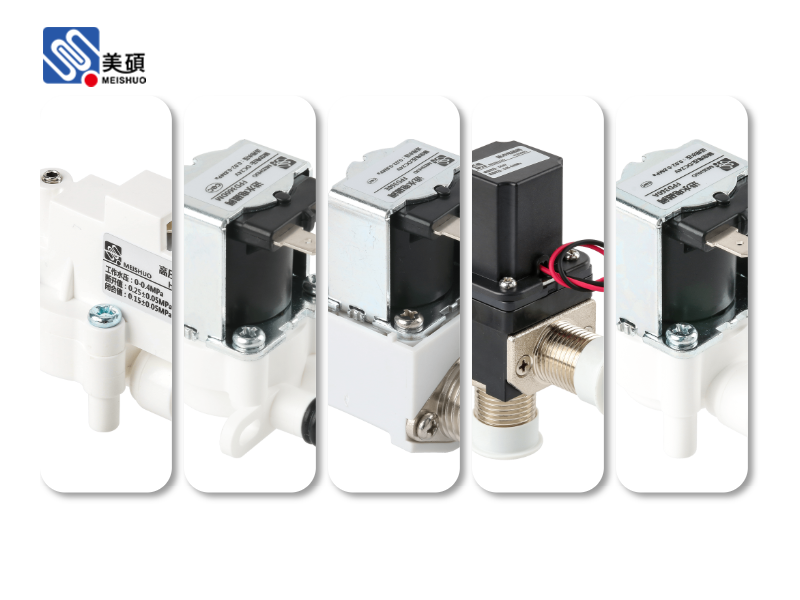
In the food and beverage industry, ensuring the highest standards of safety and hygiene is paramount. One crucial component that plays a vital role in maintaining these standards is the food grade solenoid valve. This article delves into the importance of food grade solenoid valve certification, its significance in the industry, and how it ensures the quality and safety of food products.
**Introduction**
Food grade solenoid valves are essential in various applications within the food and beverage industry, including processing, packaging, and storage. These valves are designed to handle food-grade fluids, ensuring that they do not contaminate the product. To guarantee the reliability and safety of these valves, they must undergo rigorous certification processes. This article explores the significance of food grade solenoid valve certification and its impact on the industry.
**Understanding Food Grade Solenoid Valve Certification**
Food grade solenoid valve certification is a process that ensures the valves meet specific standards and regulations set by regulatory bodies. These standards are designed to protect public health and safety by ensuring that the valves are made from safe materials, are free from contaminants, and operate reliably.
The certification process typically involves several stages, including material testing, design and manufacturing inspections, and performance testing. These tests are conducted by independent third-party organizations to ensure impartiality and objectivity.
**Significance of Food Grade Solenoid Valve Certification**
1. **Ensuring Safety and Hygiene**: The primary purpose of food grade solenoid valve certification is to ensure the safety and hygiene of food products. By adhering to strict standards, these valves help prevent contamination and maintain the quality of food products.
2. **Compliance with Regulations**: Food grade solenoid valve certification ensures compliance with various regulations and standards, such as the FDA (Food and Drug Administration) and the 3A Sanitary Standards. This compliance is crucial for businesses operating in the food and beverage industry, as it demonstrates their commitment to maintaining high safety and quality standards.
3. **Enhancing Product Quality**: Certified food grade solenoid valves are more reliable and durable, leading to improved product quality and reduced downtime. This, in turn, enhances the overall efficiency of food processing operations.
4. **Building Consumer Trust**: By using certified food grade solenoid valves, businesses can build consumer trust in their products. Consumers are more likely to purchase products from companies that prioritize safety and quality.
**How Food Grade Solenoid Valve Certification Benefits the Industry**
1. **Increased Market Access**: Companies that use certified food grade solenoid valves can access more markets, as regulatory bodies and consumers around the world recognize the importance of certification.
2. **Reduced Risk of Liability**: By ensuring that their products meet stringent safety and quality standards, businesses can reduce the risk of liability claims and legal issues.
3. **Improved Efficiency**: Certified food grade solenoid valves are designed to operate reliably and efficiently, reducing downtime and maintenance costs.
**Conclusion**
Food grade solenoid valve certification is a critical aspect of the food and beverage industry. By adhering to strict standards and regulations, these valves help ensure the safety, quality, and reliability of food products. Businesses that prioritize certification can gain a competitive edge, build consumer trust, and contribute to the overall growth and success of the industry.
 Chat Oline