The food industry is a highly regulated sector, with strict requirements for equipment used in the processing and packaging of food products. One such critical piece of equipment is the food grade solenoid valve. This article delves into the importance of food grade solenoid valves in modern food processing and their role in ensuring food safety and quality.
**Introduction**
Food grade solenoid valves are specialized devices designed to control the flow of fluids in food processing applications. They are essential for maintaining hygiene, preventing contamination, and ensuring the efficient operation of processing lines. As the food industry continues to evolve, the demand for reliable and high-quality food grade solenoid valves has increased significantly.
**Understanding Food Grade Solenoid Valves**
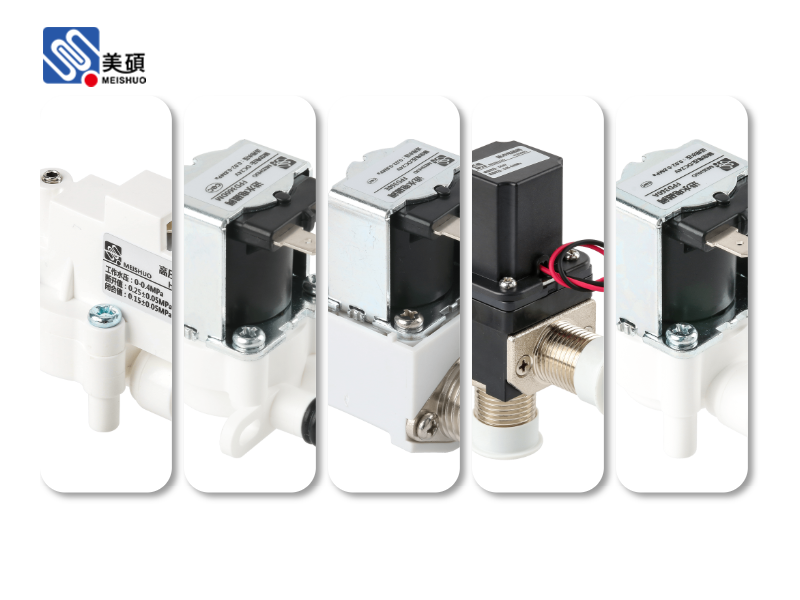
A food grade solenoid valve is a type of electromechanical device that uses an electromagnet to control the flow of fluids through a valve body. These valves are specifically designed to meet the stringent requirements of the food industry, including resistance to corrosion, high-temperature stability, and easy cleaning.
One of the key features of food grade solenoid valves is their body material. These valves are typically made from materials such as 316 stainless steel, polypropylene, or PTFE (Teflon), which are known for their corrosion resistance and non-reactive properties. This ensures that the valves do not contaminate the food product or introduce harmful substances into the processing line.
**Applications of Food Grade Solenoid Valves**
Food grade solenoid valves find applications in various stages of food processing, including:
1. **Pumping Systems**: Solenoid valves are used to control the flow of liquids, such as water, juices, and sauces, in pumping systems. This helps maintain the desired flow rate and pressure for efficient processing.
2. **Washing and Sanitizing**: In the washing and sanitizing stages, food grade solenoid valves are used to control the flow of cleaning agents and water, ensuring effective cleaning and preventing the growth of bacteria and other pathogens.
3. **Packaging Machines**: Solenoid valves play a crucial role in packaging machines, controlling the flow of food products, such as liquids, powders, and granulates, into packaging containers.
4. **Cooling and Heating Systems**: In cooling and heating systems, food grade solenoid valves are used to control the flow of fluids, such as water and oil, to maintain the desired temperature for food processing.
**Advantages of Food Grade Solenoid Valves**
Several advantages make food grade solenoid valves the preferred choice in the food industry:
1. **Hygiene and Safety**: These valves are designed to prevent contamination and ensure food safety, making them ideal for use in food processing applications.
2. **Efficiency**: Food grade solenoid valves offer precise control over fluid flow, leading to improved efficiency in processing operations.
3. **Reliability**: These valves are durable and reliable, ensuring consistent performance even under harsh conditions.
4. **Ease of Cleaning**: The materials used in food grade solenoid valves are easy to clean, reducing downtime and maintenance costs.
**Conclusion**
Food grade solenoid valves are an indispensable component in modern food processing. Their ability to ensure food safety, efficiency, and reliability has made them a vital tool in the food industry. As the industry continues to grow and evolve, the demand for high-quality food grade solenoid valves is expected to rise, further highlighting their importance in the food processing sector.
 Chat Oline