In the highly regulated food industry, the use of high-quality equipment is crucial to ensure the safety and quality of products. One such critical component is the Food Grade Solenoid Valve. This article delves into the significance of Food Grade Solenoid Valves in the food industry, their features, and why they are indispensable in various applications.
The food industry operates under stringent hygiene and safety standards to protect consumers from contamination and maintain product integrity. Food Grade Solenoid Valves play a pivotal role in this process by controlling the flow of fluids, ensuring that they remain uncontaminated and safe for consumption.
**Features of Food Grade Solenoid Valves**
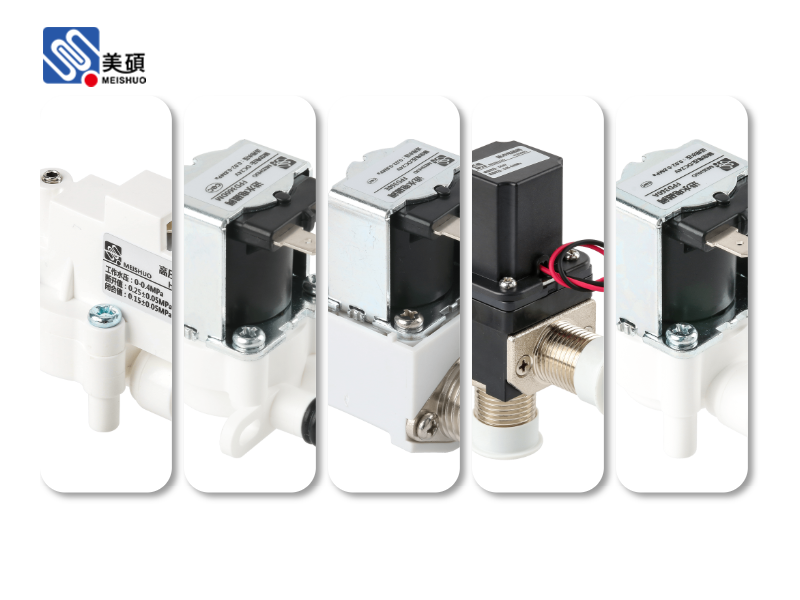
Food Grade Solenoid Valves are designed with specific features that make them ideal for use in the food industry. Some of these features include:
1. **Material Compatibility**: These valves are made from materials that are non-toxic and resistant to corrosion, such as stainless steel and plastic. This ensures that they do not leach harmful substances into the food or beverages they come into contact with.
2. **Seal Technology**: Food Grade Solenoid Valves use specialized seals that prevent leaks and cross-contamination. These seals are made from food-grade materials and are designed to withstand high temperatures and pressures, ensuring long-lasting performance.
3. **Easy Cleaning and Sanitization**: The design of these valves allows for easy cleaning and sanitization, which is essential in maintaining a hygienic environment in food processing facilities.
4. **Robust Construction**: Food Grade Solenoid Valves are built to withstand harsh conditions, including extreme temperatures and aggressive chemicals, making them durable and reliable.
**Applications of Food Grade Solenoid Valves**
Food Grade Solenoid Valves are used in various applications across the food industry, including:
1. **Beverage Production**: These valves are used to control the flow of liquids, such as water, juice, and beer, during the production process.
2. **Food Processing**: They are essential in controlling the flow of ingredients, such as spices, flour, and sugar, in food processing facilities.
3. **Packaging**: Food Grade Solenoid Valves are used in packaging machines to control the flow of liquids and gases, ensuring that products are sealed properly and safely.
4. **Washing and Sanitization**: These valves are used in washing and sanitization systems to control the flow of cleaning agents and water, ensuring that equipment and surfaces are thoroughly cleaned.
**Benefits of Using Food Grade Solenoid Valves**
The use of Food Grade Solenoid Valves in the food industry offers several benefits, including:
1. **Enhanced Safety**: By preventing contamination and maintaining product integrity, these valves contribute to the safety of food and beverages.
2. **Improved Efficiency**: The reliable performance of Food Grade Solenoid Valves helps to optimize production processes, leading to increased efficiency.
3. **Cost Savings**: By reducing the risk of product recalls and waste, these valves can help businesses save money in the long run.
4. **Regulatory Compliance**: The use of Food Grade Solenoid Valves helps businesses meet the stringent hygiene and safety standards set by regulatory bodies.
In conclusion, Food Grade Solenoid Valves are an essential component in the food industry, providing reliable and safe control of fluid flow. Their unique features and applications make them indispensable in maintaining the quality and safety of food and beverages.
 Chat Oline