In the intricate world of food processing, the choice of equipment and components is paramount to ensure the safety, quality, and efficiency of the final product. One such critical component is the Food Grade Solenoid Valve. This article delves into the significance of Food Grade Solenoid Valves in modern food processing, their features, benefits, and how they contribute to the overall quality assurance of the food industry.
The food industry operates under stringent regulations and standards to ensure consumer safety. Among these standards, the use of food-grade materials is crucial. Food Grade Solenoid Valves are specifically designed to meet these stringent requirements, making them an indispensable part of modern food processing facilities.
**Understanding Food Grade Solenoid Valves**
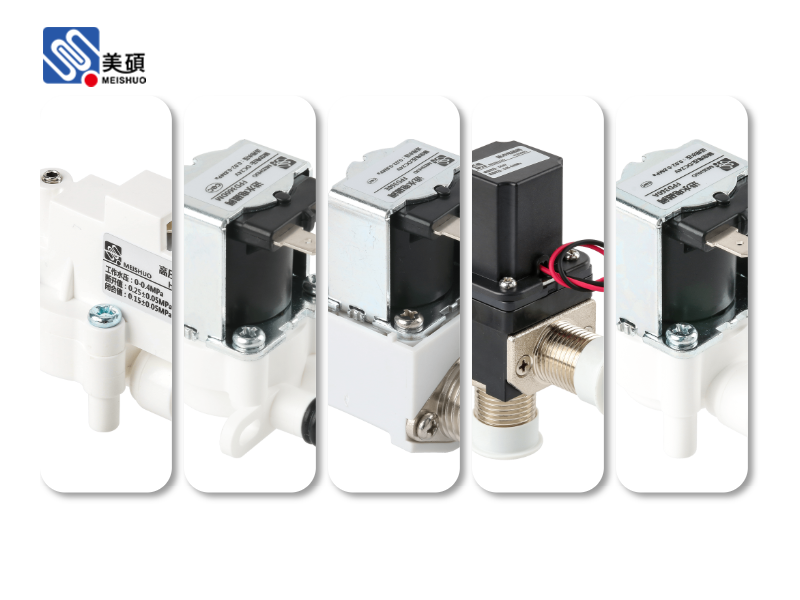
Food Grade Solenoid Valves are electromagnetic valves designed for use in food and beverage processing applications. They are constructed using materials that are safe for contact with food, ensuring that no harmful substances leach into the product. These valves are typically made from materials such as stainless steel, polypropylene, and FDA-approved plastics.
**Key Features of Food Grade Solenoid Valves**
1. **Material Compliance**: The primary feature of Food Grade Solenoid Valves is their compliance with food-grade materials. This ensures that the valves do not contaminate the food product or the processing environment.
2. **Sanitization**: Food processing facilities require frequent sanitization to prevent the growth of bacteria and other pathogens. Food Grade Solenoid Valves are designed to be easily sanitized, with smooth surfaces and no crevices where contaminants can hide.
3. **Durable Construction**: These valves are built to withstand the harsh conditions of food processing environments, including high temperatures, aggressive cleaning chemicals, and constant use.
4. **Precision and Reliability**: Food Grade Solenoid Valves offer precise control over the flow of liquids and gases, ensuring consistent quality in the final product. Their reliable operation is crucial in maintaining production schedules and preventing product defects.
**Benefits of Using Food Grade Solenoid Valves**
1. **Enhanced Food Safety**: By using food-grade materials and designs, Food Grade Solenoid Valves minimize the risk of contamination, thereby enhancing food safety.
2. **Improved Product Quality**: The precise control and reliable operation of these valves contribute to the consistency and quality of the final product.
3. **Cost-Effective**: Although Food Grade Solenoid Valves may have a higher initial cost compared to standard valves, their durability and reduced maintenance requirements make them a cost-effective choice in the long run.
4. **Regulatory Compliance**: The use of Food Grade Solenoid Valves helps food processing facilities meet regulatory requirements and maintain certifications.
**Applications of Food Grade Solenoid Valves**
Food Grade Solenoid Valves find applications in various stages of food processing, including:
1. **Pumping and Transfer**: Controlling the flow of liquids during pumping and transfer operations. 2. **Sanitization**: Activating cleaning cycles in sanitization systems. 3. **Packaging**: Controlling the flow of gases and liquids during packaging processes. 4. **Process Control**: Regulating the flow of ingredients and additives in processing lines.
**Conclusion**
Food Grade Solenoid Valves play a crucial role in ensuring the safety, quality, and efficiency of modern food processing facilities. Their use not only enhances food safety but also contributes to improved product quality and regulatory compliance. As the food industry continues to evolve, the demand for Food Grade Solenoid Valves is expected to grow, making them an essential component in the quest for safe and high-quality food products.
 Chat Oline