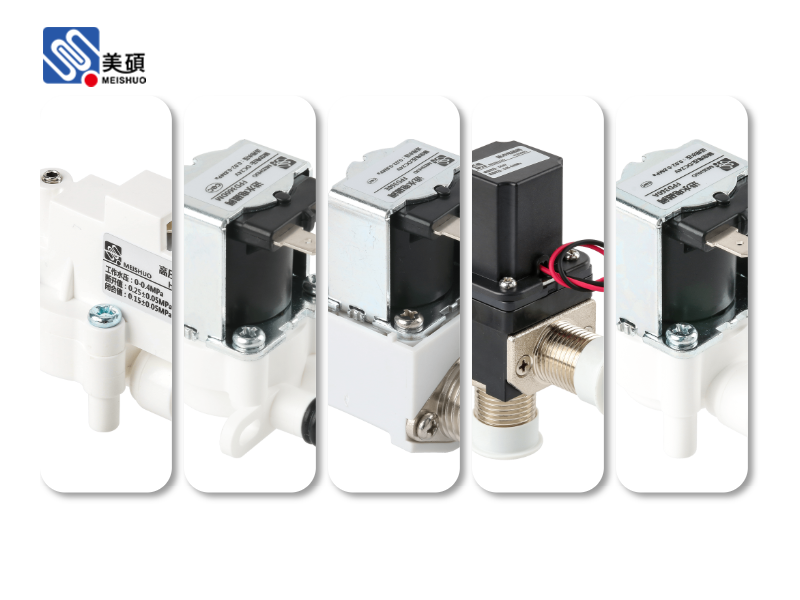
The RoHS compliant solenoid valve is an essential component in many industries, ensuring environmental safety and compliance with stringent regulations. In this article, we will delve into what makes a solenoid valve RoHS compliant, its applications, and the benefits of using such valves.
**Introduction**
The RoHS Directive, also known as the Restriction of Hazardous Substances Directive, is a European Union directive that restricts the use of certain hazardous substances in electrical and electronic equipment. The RoHS compliant solenoid valve is designed to meet these standards, ensuring that it does not contain any of the restricted substances, such as lead, cadmium, mercury, hexavalent chromium, polybrominated biphenyls (PBBs), and polybrominated diphenyl ethers (PBDEs).
**What Makes a Solenoid Valve RoHS Compliant?**
A RoHS compliant solenoid valve is made from materials that do not contain any of the restricted substances. This includes the valve body, the coil, and any other components that come into contact with the fluid being controlled. Manufacturers of RoHS compliant solenoid valves undergo rigorous testing to ensure that their products meet the directive's requirements.
**Applications of RoHS Compliant Solenoid Valves**
RoHS compliant solenoid valves are used in a wide range of applications, including:
1. **Automotive Industry**: In the automotive sector, these valves are used in engine management systems, air conditioning, and power steering. 2. **Food and Beverage Industry**: They are employed in beverage dispensing systems, water purification, and food processing equipment. 3. **Pharmaceutical Industry**: Solenoid valves are used in pharmaceutical manufacturing processes, such as filling and dispensing systems. 4. **Chemical Industry**: These valves are used in chemical processing plants for controlling the flow of hazardous materials. 5. **Environmental Protection**: They are used in wastewater treatment plants and other environmental protection systems.
**Benefits of Using RoHS Compliant Solenoid Valves**
There are several benefits to using RoHS compliant solenoid valves:
1. **Environmental Safety**: By not containing hazardous substances, these valves help to protect the environment and human health. 2. **Regulatory Compliance**: Using RoHS compliant valves ensures that your products meet the requirements of the RoHS Directive, avoiding potential fines and legal issues. 3. **Longevity**: The absence of hazardous substances in these valves can lead to longer lifespan and reduced maintenance costs. 4. **Cost-Effective**: Although RoHS compliant solenoid valves may have a higher initial cost, their long-term benefits can result in significant cost savings.
**Conclusion**
In conclusion, the RoHS compliant solenoid valve is an essential component in many industries, offering environmental safety, regulatory compliance, and cost savings. As the demand for environmentally friendly products continues to grow, the importance of RoHS compliant solenoid valves will only increase.
 Chat Oline