In the food processing industry, the integrity and safety of equipment are paramount. One critical component that plays a vital role in ensuring product safety and quality is the food grade solenoid valve. These valves are designed to withstand the stringent requirements of the food industry, and their certification is a testament to their reliability. This article delves into the importance of food grade solenoid valve certification, the certification process, and the benefits it offers to both manufacturers and end-users.
**Introduction**
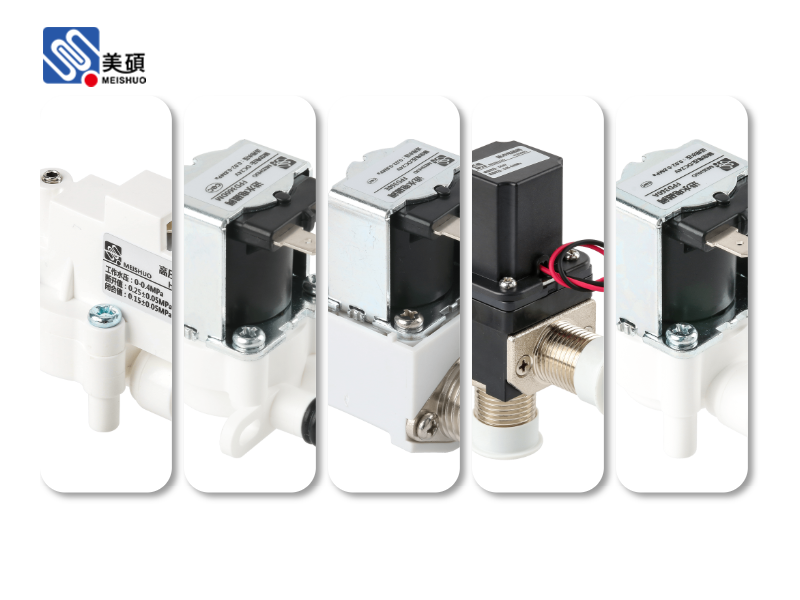
The food grade solenoid valve is an essential part of many food processing systems, responsible for controlling the flow of fluids such as water, oil, and other liquids. Given the critical nature of these valves in maintaining food safety, it is imperative that they meet stringent standards. Food grade solenoid valve certification ensures that these valves are fit for purpose and comply with the necessary regulations.
**Why Food Grade Solenoid Valve Certification Matters**
1. **Regulatory Compliance**: Food grade solenoid valves must adhere to specific regulations and standards, such as the FDA (Food and Drug Administration) guidelines in the United States or the EU's Regulation (EC) No 1935/2004. Certification ensures that these valves meet these requirements.
2. **Safety and Quality Assurance**: Certification processes involve rigorous testing to ensure that the valves are free from contaminants and can withstand the harsh conditions of the food processing environment. This guarantees the safety and quality of the end product.
3. **Consumer Trust**: In an industry where consumer health and safety are paramount, certification serves as a trust signal to both consumers and regulatory bodies, assuring them of the valve's reliability.
**The Certification Process**
1. **Material Selection**: The first step in the certification process is the selection of materials. Food grade solenoid valves must be made from materials that are safe for contact with food, such as stainless steel, polypropylene, or PTFE.
2. **Design and Construction**: The design and construction of the valve must be in compliance with the relevant standards. This includes the valve's body, diaphragm, and other components.
3. **Testing**: The valve undergoes a series of tests to ensure its performance and durability. These tests may include pressure testing, leakage testing, and material analysis.
4. **Documentation**: Certification requires comprehensive documentation, including test results, material specifications, and manufacturing processes.
**Benefits of Food Grade Solenoid Valve Certification**
1. **Enhanced Marketability**: Manufacturers of certified food grade solenoid valves can use the certification as a marketing tool to differentiate their products from non-certified alternatives.
2. **Longer Product Lifespan**: Certified valves are designed to withstand the harsh conditions of the food processing environment, leading to a longer lifespan and reduced maintenance costs.
3. **Improved Efficiency**: By ensuring that the valves operate reliably, certification can lead to improved efficiency in food processing operations.
**Conclusion**
Food grade solenoid valve certification is a crucial step in ensuring the safety and quality of food processing equipment. By adhering to stringent standards, manufacturers can provide their customers with a reliable and safe product. For end-users, certification serves as a guarantee of the valve's performance and compliance with regulatory requirements. As the food industry continues to evolve, the importance of food grade solenoid valve certification will only grow, making it a vital consideration for all stakeholders.
 Chat Oline