In the ever-evolving world of food processing, maintaining the highest standards of hygiene and efficiency is paramount. One of the key components that play a crucial role in achieving these standards is the Food Grade Solenoid Valve. This article delves into the importance of these valves, their working principles, and how they contribute to the safety and quality of food products.
**Introduction**
The food industry is highly regulated, and for good reason. Ensuring that food products are safe for consumption is a top priority for manufacturers, regulators, and consumers alike. Food Grade Solenoid Valves are specifically designed to meet these stringent requirements, providing a reliable and hygienic solution for controlling the flow of fluids in food processing systems.
**Understanding Food Grade Solenoid Valves**
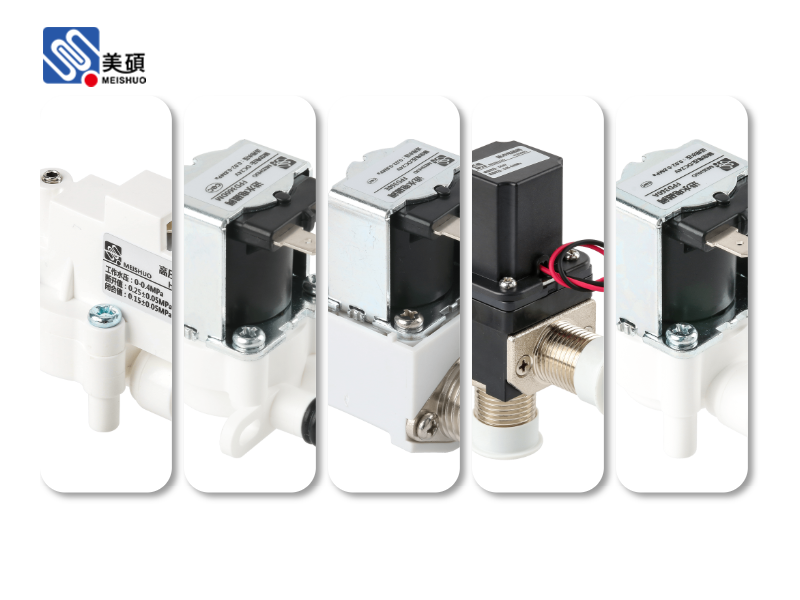
Food Grade Solenoid Valves are electromechanical devices that control the flow of fluids, such as water, air, and various chemicals, in food processing systems. These valves are constructed from materials that are safe for use in food and beverage applications, ensuring that they do not contaminate the product.
The primary components of a Food Grade Solenoid Valve include:
- **Body**: The body is the main part of the valve, and it is typically made from materials such as stainless steel, polypropylene, or PVDF. These materials are chosen for their resistance to corrosion and their ability to withstand the harsh conditions of food processing environments.
- **Diaphragm**: The diaphragm is a flexible membrane that separates the valve's two ports. It is made from materials such as silicone or PTFE, which are inert and non-reactive to food products.
- **Solenoid**: The solenoid is the electrical component that controls the valve's operation. When an electrical current is applied, the solenoid pulls the diaphragm, allowing fluid to flow through the valve. When the current is removed, the diaphragm returns to its original position, closing the valve.
**The Importance of Food Grade Solenoid Valves in Food Processing**
1. **Hygiene**: One of the most critical aspects of food processing is maintaining a clean and hygienic environment. Food Grade Solenoid Valves are designed to minimize the risk of contamination, as they are made from materials that are resistant to bacteria and other microorganisms.
2. **Efficiency**: These valves are highly efficient, allowing for quick and precise control of fluid flow. This efficiency translates to reduced downtime and increased productivity in food processing operations.
3. **Safety**: Food Grade Solenoid Valves are designed to operate in harsh environments, ensuring that they remain functional even under extreme conditions. This reliability is crucial for maintaining the safety of food products.
4. **Regulatory Compliance**: The use of Food Grade Solenoid Valves helps food manufacturers comply with regulatory requirements, such as those set forth by the FDA and the European Union.
**Conclusion**
Food Grade Solenoid Valves are an essential component of modern food processing systems. Their ability to provide reliable, efficient, and hygienic control of fluid flow makes them a crucial tool for food manufacturers looking to maintain the highest standards of quality and safety. As the food industry continues to evolve, the importance of these valves will only grow, ensuring that consumers can enjoy safe and delicious food products for years to come.
 Chat Oline