In the world of industrial automation, the food grade solenoid valve stands as a cornerstone of efficiency and reliability. This specialized component plays a crucial role in the food and beverage industry, ensuring the safe and hygienic handling of products. This article delves into the intricacies of food grade solenoid valves, exploring their design, applications, and the benefits they offer.
**Introduction**
The food grade solenoid valve is a type of electromagnetic valve specifically designed for use in food processing and beverage manufacturing. These valves are engineered to meet stringent hygiene standards, making them ideal for applications where product safety and cleanliness are paramount. Unlike standard solenoid valves, food grade valves are constructed from materials that are non-toxic, corrosion-resistant, and easy to clean.
**Design and Materials**
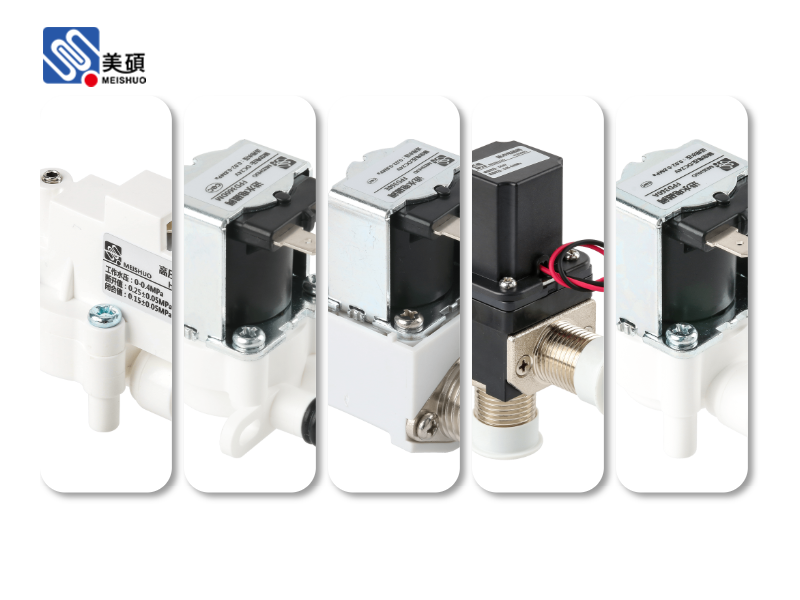
The design of a food grade solenoid valve is focused on minimizing the risk of contamination. Key components, such as the body, diaphragm, and seals, are made from materials that comply with food safety regulations. Common materials include stainless steel, polypropylene, and FDA-approved elastomers. These materials not only ensure the valve's durability but also its compatibility with a wide range of food products.
One of the standout features of food grade solenoid valves is their ability to withstand harsh cleaning agents and high temperatures. This makes them suitable for use in applications involving steam cleaning and high-pressure water jet cleaning. The valves are also designed with a compact and modular construction, allowing for easy installation and maintenance.
**Applications**
Food grade solenoid valves find extensive applications across the food and beverage industry. Some of the most common uses include:
1. **Pumping Systems**: These valves are often used in pumping systems to control the flow of liquids, such as water, juices, and sauces. 2. **Filling Machines**: In filling operations, food grade solenoid valves ensure precise control of the product flow, reducing waste and improving efficiency. 3. **CIP Systems**: Clean-in-place (CIP) systems use food grade solenoid valves to automate the cleaning process, ensuring that equipment is thoroughly sanitized. 4. **Packaging Machines**: These valves are used in packaging machines to control the flow of products into containers, such as bottles and cans.
**Benefits**
The use of food grade solenoid valves offers several benefits, including:
1. **Hygiene**: The materials and design of these valves minimize the risk of contamination, ensuring the safety of food products. 2. **Efficiency**: These valves provide precise control over the flow of products, improving overall efficiency and reducing waste. 3. **Durability**: Constructed from high-quality materials, food grade solenoid valves are designed to withstand harsh conditions, ensuring long-term reliability. 4. **Ease of Maintenance**: The modular design of these valves makes them easy to maintain and repair, reducing downtime and costs.
**Conclusion**
In conclusion, the food grade solenoid valve is a vital component in the food and beverage industry. Its specialized design and materials make it an ideal choice for applications where product safety and cleanliness are critical. As the industry continues to evolve, the demand for reliable and efficient food grade solenoid valves is only expected to grow. By understanding the benefits and applications of these valves, businesses can ensure the smooth operation of their production processes and the safety of their products.
 Chat Oline