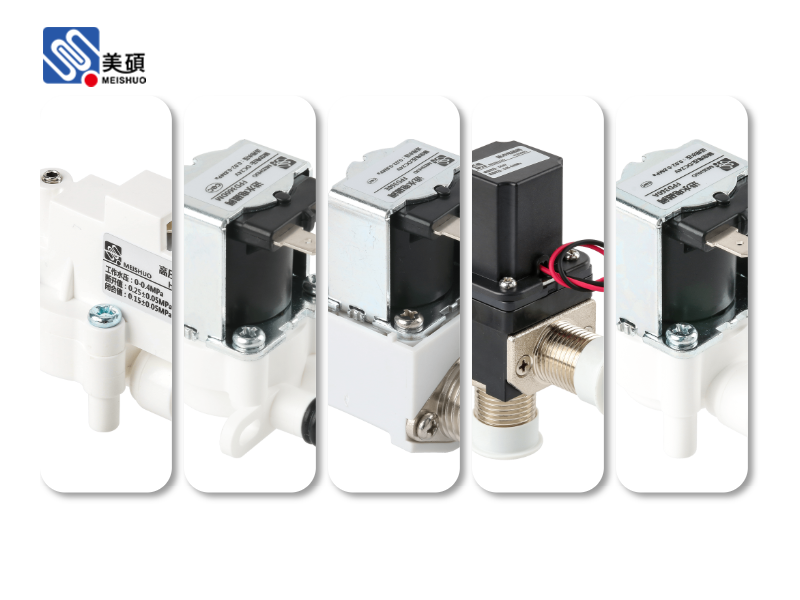
The food industry is a highly regulated sector, and the equipment used in its operations must meet strict hygiene standards. One such essential component is the Food Grade Solenoid Valve. This article delves into the role, advantages, and applications of Food Grade Solenoid Valves in modern food processing.
Introduction: In the food industry, the safety and quality of products are paramount. To ensure this, all equipment used in processing, handling, and packaging must adhere to stringent hygiene standards. Among these, Food Grade Solenoid Valves play a crucial role in maintaining the integrity and purity of food products.
Role of Food Grade Solenoid Valve: Food Grade Solenoid Valves are designed specifically for use in food processing applications. They are used to control the flow of liquids, gases, and slurries in food processing systems. These valves are crucial in various processes such as mixing, blending, sterilization, and packaging.
One of the primary roles of Food Grade Solenoid Valves is to prevent cross-contamination. They are made from materials that are safe for food contact and do not leach harmful substances into the product. This ensures that the final product is safe for consumption.
Advantages of Food Grade Solenoid Valves:
1. Hygiene: Food Grade Solenoid Valves are made from materials that are non-toxic and resistant to corrosion. They are easy to clean and sanitize, making them ideal for use in food processing environments.
2. Durability: These valves are designed to withstand harsh conditions, including high temperatures and pressures. This durability ensures that they can last for years without requiring frequent maintenance or replacement.
3. Precision: Food Grade Solenoid Valves offer precise control over the flow of fluids, ensuring consistent quality in the final product.
4. Energy Efficiency: These valves are designed to minimize energy consumption, reducing operating costs for food processing facilities.
Applications of Food Grade Solenoid Valves:
1. Brewing Industry: Food Grade Solenoid Valves are used in brewing processes to control the flow of liquids and gases, ensuring the quality of beer and other alcoholic beverages.
2. Dairy Industry: These valves are used in milk processing plants to control the flow of milk and other dairy products, ensuring their safety and quality.
3. Meat Processing: Food Grade Solenoid Valves are used in meat processing facilities to control the flow of liquids and gases during processing, packaging, and sterilization.
4. Beverage Industry: These valves are used in beverage production to control the flow of liquids and gases, ensuring the quality of the final product.
Conclusion: Food Grade Solenoid Valves are an essential component in the food processing industry. Their role in maintaining hygiene, durability, precision, and energy efficiency cannot be overstated. As the food industry continues to evolve, the demand for high-quality, reliable Food Grade Solenoid Valves will only increase.
 Chat Oline