In the food and beverage industry, ensuring the safety and quality of products is paramount. One crucial component that plays a significant role in maintaining these standards is the food grade solenoid valve. This article delves into the concept of food grade solenoid valve certification, its importance, and how it ensures the integrity of the products we consume.
**Introduction**
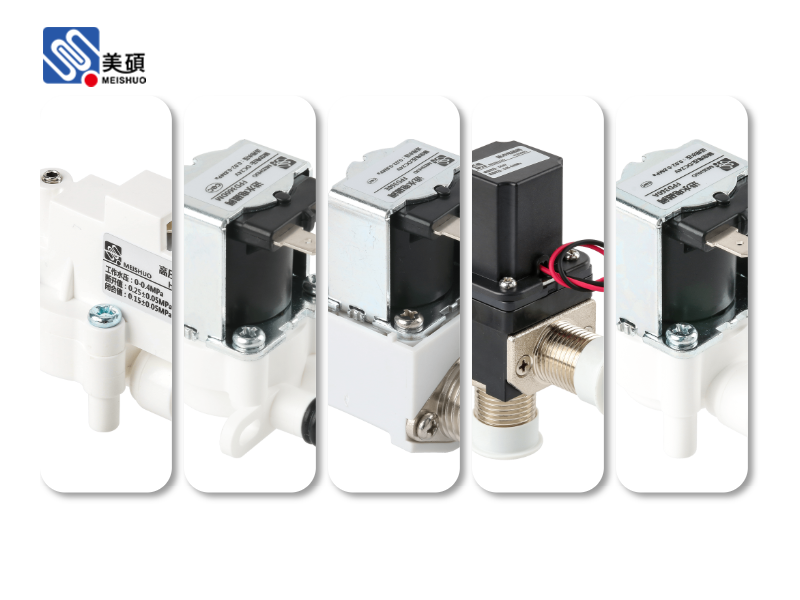
The food grade solenoid valve is a critical piece of equipment used in various applications within the food and beverage industry. These valves are designed to control the flow of fluids, such as water, chemicals, and gases, in a manner that is safe and hygienic. Food grade solenoid valve certification is a process that guarantees these valves meet specific standards and regulations, ensuring they are suitable for use in food processing environments.
**What is Food Grade Solenoid Valve Certification?**
Food grade solenoid valve certification is a process by which these valves are tested and evaluated to ensure they meet the required safety and hygiene standards. This certification is typically awarded by recognized certification bodies, which adhere to international standards such as ISO 22000, FDA, and 3A Sanitary Standards.
**Importance of Food Grade Solenoid Valve Certification**
1. **Safety and Hygiene**: The primary reason for food grade solenoid valve certification is to ensure the safety and hygiene of food products. These valves are designed to prevent contamination and maintain the integrity of the products they handle.
2. **Regulatory Compliance**: Many countries have specific regulations governing the use of equipment in the food industry. Food grade solenoid valve certification ensures that these valves comply with these regulations, helping manufacturers avoid legal issues and penalties.
3. **Consumer Trust**: Consumers are increasingly concerned about the safety and quality of the food they consume. Food grade solenoid valve certification provides a level of assurance that the products have been manufactured using safe and reliable equipment, thereby building consumer trust.
**Certification Process**
The certification process for food grade solenoid valves involves several stages:
1. **Material Selection**: The materials used in the construction of these valves must be non-toxic and safe for use in food processing environments.
2. **Design and Construction**: The design and construction of the valves must be such that they can withstand the harsh conditions of food processing, including temperature extremes and exposure to chemicals.
3. **Testing**: The valves are subjected to rigorous testing to ensure they meet the required performance standards. This includes testing for leakage, durability, and resistance to corrosion.
4. **Documentation**: The manufacturer must provide detailed documentation of the valve's design, materials, and testing results.
**Benefits of Using Certified Food Grade Solenoid Valves**
1. **Improved Product Quality**: Using certified food grade solenoid valves can lead to improved product quality, as these valves are designed to minimize contamination and maintain the integrity of the products.
2. **Reduced Maintenance Costs**: Certified valves are typically more durable and require less maintenance, leading to cost savings for manufacturers.
3. **Enhanced Reputation**: By using certified valves, manufacturers can enhance their reputation as a provider of safe and high-quality products.
**Conclusion**
Food grade solenoid valve certification is a critical process that ensures the safety and quality of products in the food and beverage industry. By adhering to international standards and rigorous testing procedures, manufacturers can provide consumers with products that they can trust. As the demand for safe and hygienic food continues to grow, the importance of food grade solenoid valve certification will only increase.
 Chat Oline