In the world of industrial automation, the food grade solenoid valve stands out as a crucial component for ensuring the safety and quality of food processing. This article delves into the intricacies of food grade solenoid valves, exploring their design, applications, and benefits in the food and beverage industry.
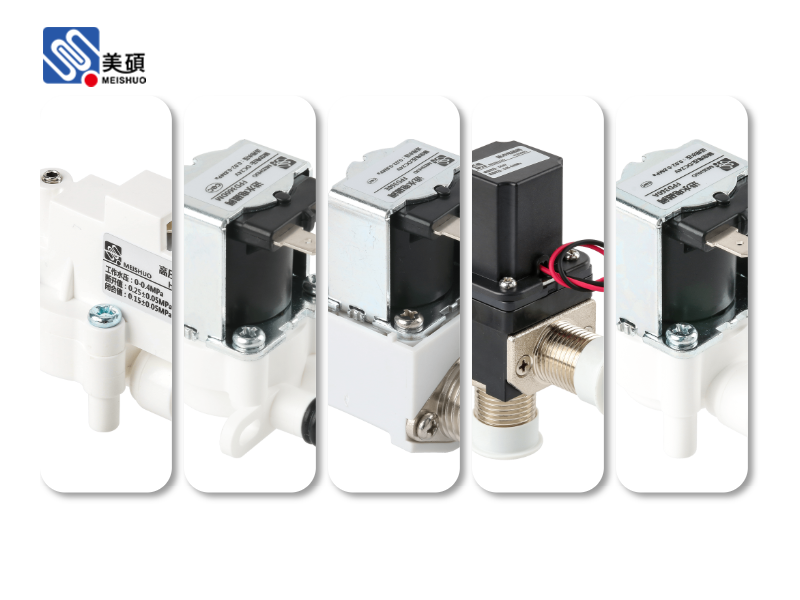
The food grade solenoid valve is a type of valve designed specifically for use in food processing and handling applications. These valves are constructed with materials that meet stringent hygiene and safety standards, making them ideal for use in environments where cleanliness and purity are paramount. Let's explore the key aspects of food grade solenoid valves.
**Design and Materials**
The design of a food grade solenoid valve is focused on minimizing the risk of contamination. These valves are typically made from materials such as stainless steel, polypropylene, and PTFE (Teflon), which are known for their resistance to corrosion and heat. The surfaces of these materials are smooth to prevent the accumulation of bacteria and other microorganisms, ensuring that the valve remains hygienic throughout its lifespan.
The internal components of food grade solenoid valves are also designed to minimize the potential for contamination. For instance, the seals and gaskets are made from food-grade materials that do not leach harmful substances into the food or beverage being processed. This attention to detail is crucial in maintaining the quality and safety of the end product.
**Applications in the Food and Beverage Industry**
Food grade solenoid valves find a wide range of applications in the food and beverage industry. Some of the most common uses include:
1. **Water Treatment**: These valves are used to control the flow of water in water treatment systems, ensuring that the water used in food processing is clean and safe. 2. **Sanitary Processes**: They are essential in sanitizing processes, such as cleaning in place (CIP) systems, where valves need to be disassembled and cleaned thoroughly. 3. **Packaging**: Food grade solenoid valves are used in packaging machines to control the flow of ingredients and packaging materials. 4. **Pumping Systems**: They are employed in pumping systems to control the flow of liquids, ensuring that the correct amount of product is delivered to the desired location.
**Benefits of Food Grade Solenoid Valves**
There are several benefits to using food grade solenoid valves in food processing applications:
1. **Hygiene**: The materials and design of these valves ensure that they are suitable for use in food processing environments, minimizing the risk of contamination. 2. **Durability**: Food grade solenoid valves are constructed from high-quality materials that are resistant to corrosion and heat, ensuring a long lifespan. 3. **Precision**: These valves offer precise control over the flow of liquids, which is crucial in food processing applications. 4. **Ease of Cleaning**: The design of food grade solenoid valves makes them easy to clean, reducing downtime and maintenance costs.
**Conclusion**
The food grade solenoid valve is a vital component in the food and beverage industry, providing a reliable and hygienic solution for controlling the flow of liquids. With their focus on safety, precision, and durability, these valves play a crucial role in ensuring the quality and safety of food products. As the demand for high-quality and safe food continues to grow, the importance of food grade solenoid valves in the food processing industry will only increase.
 Chat Oline