In the world of industrial automation, the food grade solenoid valve stands as a crucial component in ensuring the safety and efficiency of food processing systems. This article delves into the intricacies of food grade solenoid valves, their applications, and the benefits they offer in the food industry.
**Introduction**
The food industry operates under stringent regulations to ensure the safety and quality of its products. As such, the equipment used in food processing must meet high hygiene standards. Food grade solenoid valves are specifically designed to meet these requirements, providing a reliable and efficient solution for controlling the flow of fluids in food processing systems.
**What is a Food Grade Solenoid Valve?**
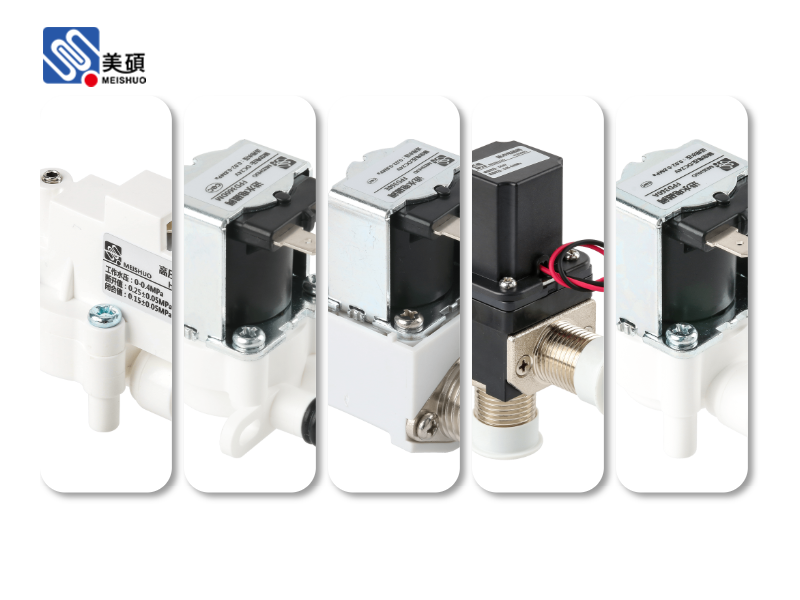
A food grade solenoid valve is a type of valve that uses an electromagnetic coil to open or close the flow of fluids. These valves are constructed from materials that are safe for use in food and beverage applications, ensuring that no harmful substances can contaminate the product.
**Materials Used in Food Grade Solenoid Valves**
The choice of materials is crucial in the construction of food grade solenoid valves. These valves are typically made from materials such as stainless steel, polypropylene, and polytetrafluoroethylene (PTFE). These materials are non-reactive, corrosion-resistant, and easy to clean, making them ideal for use in food processing environments.
**Applications of Food Grade Solenoid Valves**
Food grade solenoid valves find extensive use in various applications within the food industry. Some of the most common applications include:
1. **Beverage Industry**: Solenoid valves are used to control the flow of liquids in bottling and packaging lines, ensuring accurate dosing and preventing cross-contamination. 2. **Dairy Industry**: These valves are used to control the flow of milk and other dairy products, ensuring the hygiene and quality of the final product. 3. **Baking Industry**: Solenoid valves are used to control the flow of ingredients in mixing and baking processes, ensuring consistent product quality. 4. **Canning Industry**: These valves are used to control the flow of liquids in canning processes, ensuring the safety and quality of canned products.
**Benefits of Food Grade Solenoid Valves**
The use of food grade solenoid valves in food processing systems offers several benefits:
1. **Hygiene**: The materials used in these valves are non-reactive and easy to clean, ensuring that no harmful substances can contaminate the product. 2. **Reliability**: Food grade solenoid valves are designed to operate in harsh environments, ensuring consistent performance and longevity. 3. **Efficiency**: These valves provide precise control over the flow of fluids, reducing waste and improving overall efficiency. 4. **Safety**: The use of food grade materials ensures that the valves do not leach harmful substances into the product, making them safe for use in food processing systems.
**Conclusion**
Food grade solenoid valves play a vital role in the food industry, providing a reliable and efficient solution for controlling the flow of fluids in food processing systems. With their ability to meet stringent hygiene standards and ensure the safety and quality of food products, these valves are an essential component of modern food processing facilities.
 Chat Oline