In the world of industrial automation, the food grade solenoid valve stands as a cornerstone of efficiency and reliability. This article delves into the intricacies of food grade solenoid valves, exploring their applications, benefits, and why they are indispensable in the food and beverage industry.
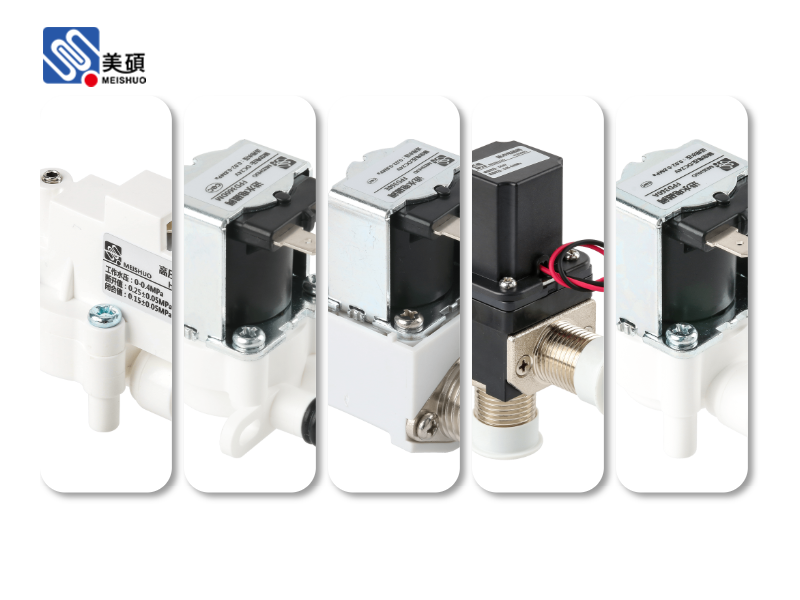
The food grade solenoid valve is a type of electromagnetic valve designed for use in environments where hygiene and safety are paramount. These valves are specifically engineered to withstand the harsh conditions of food processing, ensuring that the end product remains uncontaminated and safe for consumption.
One of the primary applications of food grade solenoid valves is in the food and beverage industry. They are used in a variety of processes, including filling, sealing, and dispensing. For instance, in bottling plants, these valves are used to control the flow of liquids into bottles, ensuring accuracy and consistency. In dairy processing, they help in regulating the flow of milk and other dairy products, maintaining their quality and safety.
The design of food grade solenoid valves is a testament to engineering excellence. They are constructed with materials that are resistant to corrosion, such as stainless steel and PTFE (Teflon). This not only ensures their longevity but also their ability to withstand the aggressive chemicals and high temperatures often encountered in food processing environments.
One of the key benefits of food grade solenoid valves is their ability to provide precise control over the flow of fluids. This is crucial in the food industry, where even the smallest variation in the flow rate can have a significant impact on the quality of the product. These valves are designed to offer tight shutoff capabilities, minimizing the risk of leaks and cross-contamination.
Moreover, food grade solenoid valves are designed to be easily sanitized. Their smooth surfaces and quick-release mechanisms make them ideal for cleaning operations, reducing the time and effort required to maintain hygiene standards. This is particularly important in the food industry, where adherence to stringent hygiene regulations is not just a legal requirement but a moral imperative.
In addition to their use in the food and beverage industry, food grade solenoid valves find applications in other sectors as well. They are used in pharmaceutical manufacturing, where they help in controlling the flow of liquids in aseptic environments. They are also used in water treatment plants, where they play a crucial role in regulating the flow of water and chemicals.
Another advantage of food grade solenoid valves is their energy efficiency. They are designed to consume minimal energy, making them an environmentally friendly choice. This not only reduces operating costs but also minimizes the carbon footprint of the facility.
In conclusion, the food grade solenoid valve is a marvel of modern engineering. Its ability to provide precise control, withstand harsh conditions, and ensure hygiene makes it an indispensable tool in the food and beverage industry. As the demand for safe and high-quality food continues to grow, the role of food grade solenoid valves in maintaining these standards cannot be overstated.
 Chat Oline