The food industry is a highly regulated sector, where safety and hygiene are paramount. One of the critical components that ensure the integrity of food products is the food grade solenoid valve. This article delves into the importance of food grade solenoid valves, their features, and how they contribute to the safety and efficiency of food processing operations.
**Introduction**
In the food industry, the use of high-quality components is essential to maintain the safety and quality of food products. Food grade solenoid valves are specifically designed to meet the stringent requirements of the food and beverage industry. These valves play a crucial role in controlling the flow of liquids, gases, and slurries in various processes, ensuring that food products remain uncontaminated and safe for consumption.
**Understanding Food Grade Solenoid Valves**
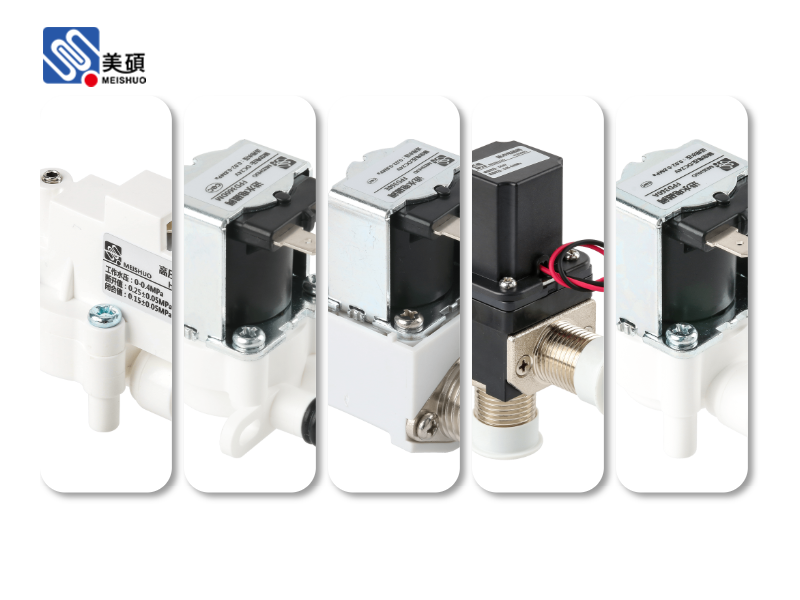
Food grade solenoid valves are designed to handle food-grade fluids, including water, milk, beer, wine, and other beverages. They are constructed with materials that are safe for use in food processing environments, such as stainless steel, polypropylene, and other non-reactive materials. These valves are designed to prevent contamination, maintain product quality, and ensure the safety of consumers.
**Key Features of Food Grade Solenoid Valves**
1. **Material Compatibility**: Food grade solenoid valves are made from materials that are safe for contact with food products. This includes stainless steel, which is resistant to corrosion and easy to clean, and plastics like polypropylene, which are non-reactive and do not leach harmful substances into the food.
2. **Sanitary Design**: These valves are designed with a focus on hygiene, featuring smooth surfaces and no dead corners where bacteria can accumulate. This makes them easy to clean and sanitize, reducing the risk of contamination.
3. **Sealing Performance**: Food grade solenoid valves are equipped with high-performance seals that prevent leaks and ensure tight shut-off. This is crucial in maintaining the quality and safety of food products.
4. **Temperature and Pressure Resistance**: These valves are designed to handle a wide range of temperatures and pressures, making them suitable for various food processing applications.
**Applications of Food Grade Solenoid Valves**
Food grade solenoid valves are used in a variety of applications within the food industry, including:
1. **Pumping Systems**: These valves are used to control the flow of liquids in pumping systems, ensuring that the correct amount of product is delivered to the desired location.
2. **Filling Machines**: In bottling and packaging operations, food grade solenoid valves are used to control the flow of liquids into bottles and containers, ensuring accurate filling and reducing waste.
3. **CIP Systems**: Clean-in-place (CIP) systems use food grade solenoid valves to control the flow of cleaning solutions, ensuring effective cleaning and sanitization of equipment.
4. **Process Control**: These valves are used in process control systems to regulate the flow of ingredients and other fluids, ensuring consistent product quality.
**Conclusion**
Food grade solenoid valves are an essential component in the food industry, providing a safe and reliable means of controlling the flow of fluids in various processes. Their material compatibility, sanitary design, and high-performance sealing make them ideal for use in food processing operations. By ensuring the integrity of food products, food grade solenoid valves play a crucial role in maintaining the safety and quality of food for consumers worldwide.
 Chat Oline