In the food and beverage industry, ensuring the highest standards of safety and hygiene is paramount. One critical component that plays a vital role in maintaining these standards is the food grade solenoid valve. This article delves into the importance of food grade solenoid valve certification, its benefits, and how it ensures the integrity of the food processing chain.
**Introduction**
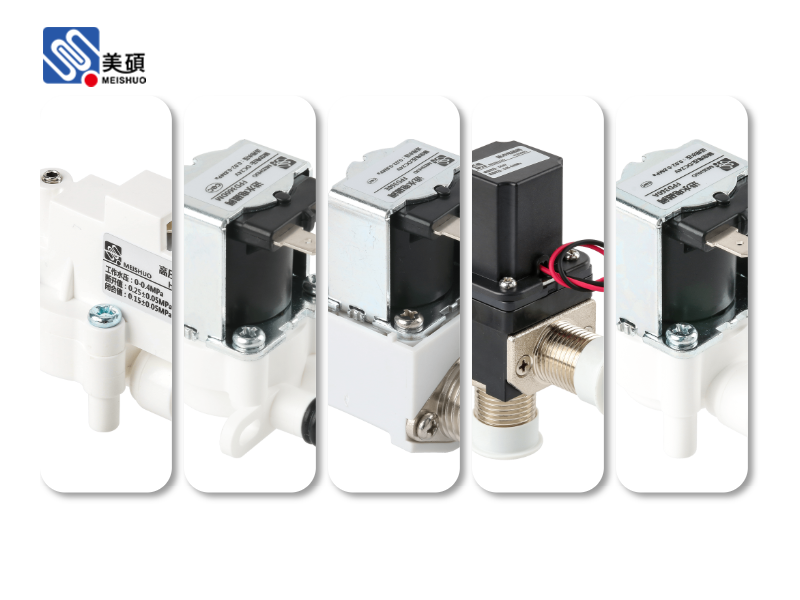
The food grade solenoid valve is a specialized piece of equipment designed to control the flow of fluids in food processing systems. These valves are subject to rigorous certification processes to guarantee their compliance with stringent hygiene and safety regulations. In this article, we will explore the significance of food grade solenoid valve certification and its impact on the food industry.
**Understanding Food Grade Solenoid Valve Certification**
Food grade solenoid valves are certified to meet specific standards set by regulatory bodies such as the 3A Sanitary Standards Inc., the European Committee for Standardization (CEN), and the International Organization for Standardization (ISO). These certifications ensure that the valves are made from materials that are safe for contact with food and are designed to prevent contamination.
**Benefits of Food Grade Solenoid Valve Certification**
1. **Enhanced Safety and Hygiene**: Certified food grade solenoid valves are made from materials that are non-toxic and resistant to corrosion, reducing the risk of contamination and ensuring the safety of the end product.
2. **Compliance with Regulations**: Certification ensures that the valves meet the required standards for use in the food and beverage industry, helping businesses avoid legal issues and penalties.
3. **Improved Product Quality**: By using certified valves, food processors can maintain consistent product quality and reduce the risk of recalls due to contamination.
4. **Increased Consumer Confidence**: Consumers are increasingly concerned about the safety and quality of the food they consume. Certified food grade solenoid valves contribute to building trust and confidence in the brand.
**The Certification Process**
The certification process for food grade solenoid valves involves several stages:
1. **Material Selection**: The materials used in the construction of the valve must be approved by the relevant regulatory bodies.
2. **Design and Manufacturing**: The valve's design must be reviewed and approved to ensure it meets the necessary standards.
3. **Testing**: The valve must undergo rigorous testing to verify its performance, durability, and resistance to contamination.
4. **Documentation**: Comprehensive documentation is required to demonstrate compliance with the certification standards.
**Conclusion**
Food grade solenoid valve certification is a crucial aspect of the food and beverage industry. By ensuring the use of certified valves, businesses can maintain the highest standards of safety, hygiene, and product quality. As the demand for safe and high-quality food continues to grow, the importance of food grade solenoid valve certification will only increase.
 Chat Oline