The RoHS compliant solenoid valve has become an essential component in various industrial applications due to its ability to ensure environmental safety and compliance with stringent regulations. In this article, we will delve into the significance of RoHS compliance in solenoid valves, their applications, and the benefits they offer to industries.
**Introduction**
The RoHS directive, also known as the Restriction of Hazardous Substances Directive, is a European Union regulation that restricts the use of certain hazardous substances in electrical and electronic equipment. The primary goal of RoHS is to protect human health and the environment from the potential dangers posed by these substances. As a result, manufacturers and suppliers of electrical and electronic products must ensure that their products are RoHS compliant.
**What is a RoHS Compliant Solenoid Valve?**
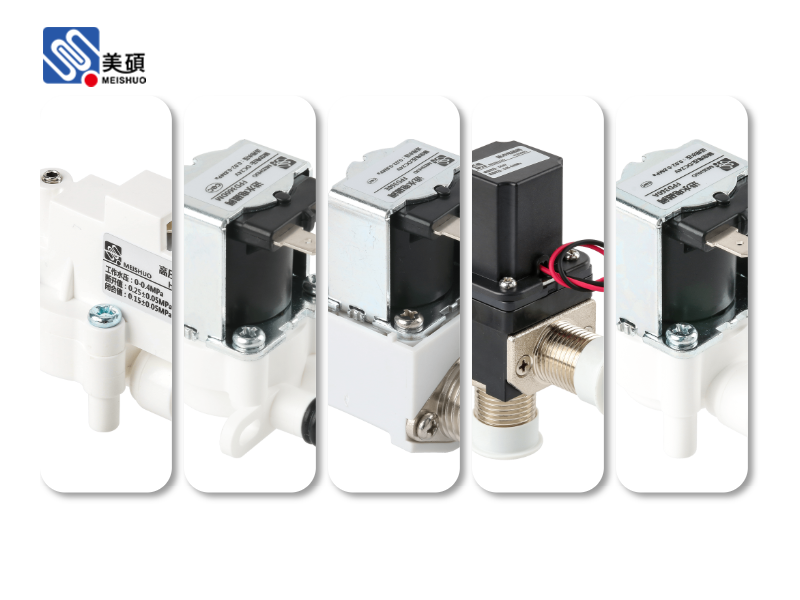
A RoHS compliant solenoid valve is a type of valve that meets the requirements of the RoHS directive. It is designed to minimize the use of hazardous substances such as lead, cadmium, mercury, hexavalent chromium, polybrominated biphenyls (PBBs), and polybrominated diphenyl ethers (PBDEs) in its construction. By adhering to these standards, RoHS compliant solenoid valves contribute to the reduction of environmental pollution and the protection of human health.
**Applications of RoHS Compliant Solenoid Valves**
RoHS compliant solenoid valves are widely used in various industries, including:
1. **Automotive Industry**: These valves are used in automotive applications such as fuel systems, air conditioning, and power steering to ensure the safety and reliability of the vehicle. 2. **Food and Beverage Industry**: In this industry, RoHS compliant solenoid valves are used in packaging and processing equipment to prevent contamination and ensure the safety of the end product. 3. **Pharmaceutical Industry**: These valves are used in pharmaceutical manufacturing processes to maintain the purity of the product and comply with regulatory requirements. 4. **Chemical Industry**: In the chemical industry, RoHS compliant solenoid valves are used in process control and safety systems to prevent accidents and ensure the safety of workers.
**Benefits of Using RoHS Compliant Solenoid Valves**
There are several benefits to using RoHS compliant solenoid valves in industrial applications:
1. **Environmental Protection**: By minimizing the use of hazardous substances, RoHS compliant solenoid valves contribute to the reduction of environmental pollution. 2. **Regulatory Compliance**: These valves ensure that industrial equipment meets the requirements of the RoHS directive, avoiding potential fines and legal issues. 3. **Safety**: RoHS compliant solenoid valves are designed to minimize the risk of accidents and health hazards, making them a safer choice for industrial applications. 4. **Longevity**: These valves are constructed with high-quality materials that are less prone to corrosion and degradation, resulting in a longer lifespan and reduced maintenance costs.
**Conclusion**
In conclusion, the RoHS compliant solenoid valve is an essential component in various industrial applications due to its ability to ensure environmental safety and compliance with stringent regulations. By choosing RoHS compliant solenoid valves, industries can contribute to the reduction of environmental pollution, ensure regulatory compliance, and enhance the safety and reliability of their equipment.
 Chat Oline