In the food processing industry, the use of high-quality equipment is paramount to ensure the safety and quality of the end products. One such critical component is the food grade solenoid valve. This article delves into the significance of food grade solenoid valve certification, its benefits, and why it is essential for the food industry.
**Introduction**
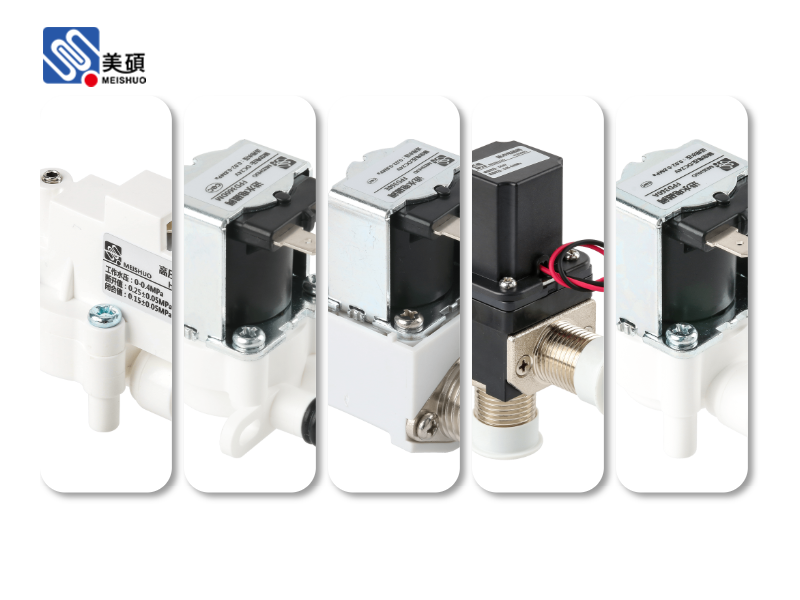
The food grade solenoid valve is a vital component in various food processing applications, including brewing, dairy, and beverage production. These valves are designed to handle food-grade fluids, ensuring that the integrity of the product is maintained throughout the manufacturing process. Food grade solenoid valve certification is a process that verifies the valve's compliance with stringent safety and quality standards. This certification process is crucial for ensuring that the valves used in the food industry are safe, reliable, and meet the required specifications.
**The Significance of Food Grade Solenoid Valve Certification**
1. **Compliance with Safety Standards**: Food grade solenoid valve certification ensures that the valves comply with international safety standards, such as ISO 8875 and FDA regulations. These standards dictate the materials used, construction, and performance requirements for valves that come into contact with food products.
2. **Hygiene and Sanitation**: The food industry operates under strict hygiene and sanitation guidelines. Food grade solenoid valves are designed to withstand regular cleaning and sterilization processes, minimizing the risk of contamination and ensuring the safety of the end product.
3. **Longevity and Reliability**: Certified food grade solenoid valves are built to last, offering a longer lifespan than non-certified counterparts. This not only reduces maintenance costs but also ensures continuous and reliable operation in critical applications.
4. **Quality Assurance**: The certification process involves rigorous testing and inspection, ensuring that the valves meet the highest quality standards. This gives food manufacturers peace of mind, knowing that their equipment is up to the task.
**Benefits of Food Grade Solenoid Valve Certification**
1. **Enhanced Product Safety**: By using certified food grade solenoid valves, food manufacturers can significantly reduce the risk of product contamination and recall, protecting their brand reputation and consumer trust.
2. **Cost Savings**: Long-term reliability and reduced maintenance requirements result in cost savings for food processing companies. Certified valves can also help avoid downtime and production losses.
3. **Regulatory Compliance**: Food grade solenoid valve certification ensures compliance with industry regulations, helping companies avoid penalties and legal issues.
4. **Global Market Access**: Many international markets require food grade equipment to be certified. By obtaining certification, food manufacturers can expand their market reach and access new markets with ease.
**Conclusion**
Food grade solenoid valve certification plays a crucial role in the food processing industry. It ensures that valves are safe, reliable, and meet the stringent requirements of the industry. By investing in certified valves, food manufacturers can protect their brand reputation, enhance product safety, and achieve regulatory compliance. In an industry where quality and safety are paramount, food grade solenoid valve certification is not just a choice but a necessity.
 Chat Oline