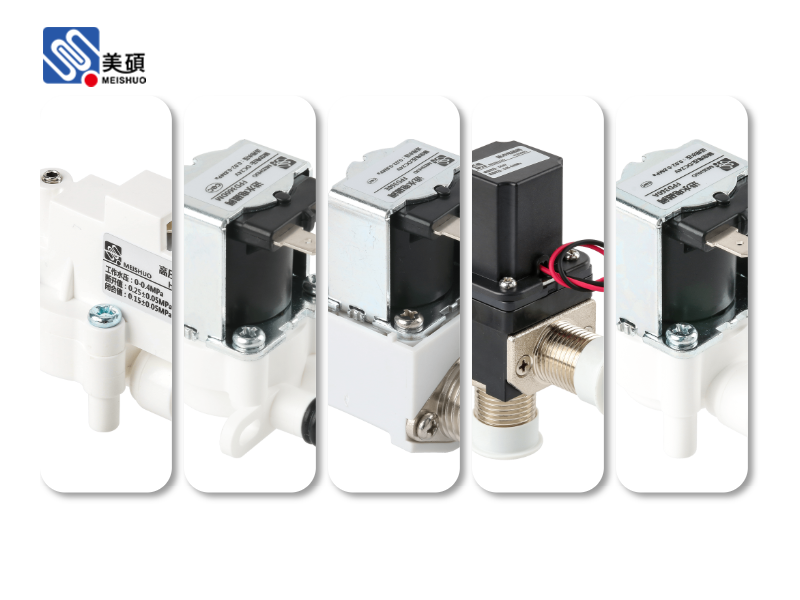
The RoHS compliant solenoid valve has become a crucial component in modern automation systems. As industries increasingly focus on environmental sustainability, the demand for RoHS compliant products has surged. This article delves into the significance of RoHS compliance in solenoid valves, their benefits, and why they are essential for sustainable automation.
**Introduction**
In the realm of automation, the solenoid valve plays a pivotal role in controlling fluid flow in various applications. These valves are electromechanical devices that use an electromagnetic coil to open or close a valve body, thereby regulating the flow of fluids. With the growing concern for environmental protection, the RoHS (Restriction of Hazardous Substances) compliant solenoid valve has emerged as a preferred choice for industries worldwide.
**What is RoHS Compliance?**
RoHS is a European Union directive that restricts the use of certain hazardous substances in electrical and electronic equipment. These substances include lead, mercury, cadmium, hexavalent chromium, polybrominated biphenyls (PBBs), and polybrominated diphenyl ethers (PBDEs). The aim of RoHS is to reduce the environmental impact of electronic waste and promote the recycling of these devices.
**Significance of RoHS Compliant Solenoid Valves**
1. Environmental Safety: By adhering to RoHS standards, solenoid valves ensure that they do not contain harmful substances that can pose a risk to the environment. This is particularly important in industries where the solenoid valves are used in close proximity to natural water sources or ecosystems.
2. Industry Regulations: Many industries, especially those operating in Europe, are required to comply with RoHS regulations. Using RoHS compliant solenoid valves helps companies meet these regulatory requirements and avoid potential fines or legal issues.
3. Customer Confidence: As consumers become more environmentally conscious, they prefer to purchase products from companies that prioritize sustainability. By using RoHS compliant solenoid valves, businesses can demonstrate their commitment to environmental responsibility, thereby enhancing customer confidence.
**Benefits of RoHS Compliant Solenoid Valves**
1. Improved Reliability: RoHS compliant solenoid valves are designed to be more durable and reliable, ensuring consistent performance over their lifespan.
2. Reduced Maintenance: These valves require less maintenance due to their robust construction and absence of hazardous materials.
3. Cost-Effective: While RoHS compliant solenoid valves may have a slightly higher upfront cost compared to non-compliant models, their long-term benefits, including reduced maintenance and operational costs, make them a cost-effective choice.
**Applications of RoHS Compliant Solenoid Valves**
RoHS compliant solenoid valves find applications in various industries, including:
1. Automotive: Used in engine cooling systems, fuel injection systems, and air conditioning systems. 2. Food and Beverage: Employed in processing and packaging facilities to ensure product safety. 3. Pharmaceutical: Utilized in manufacturing processes and packaging lines to maintain product integrity. 4. Semiconductor: Used in cleanroom environments to prevent contamination of sensitive equipment.
**Conclusion**
In conclusion, the RoHS compliant solenoid valve is an essential component in sustainable automation. By adhering to RoHS standards, these valves ensure environmental safety, meet industry regulations, and enhance customer confidence. As industries continue to prioritize sustainability, the demand for RoHS compliant solenoid valves is expected to grow, making them a crucial choice for businesses worldwide.
 Chat Oline