In the food and beverage industry, ensuring the highest standards of safety and quality is paramount. One critical component that plays a vital role in maintaining these standards is the food grade solenoid valve. This article delves into the importance of food grade solenoid valve certification, its significance in the industry, and the key factors to consider when selecting a certified valve.
**Introduction**
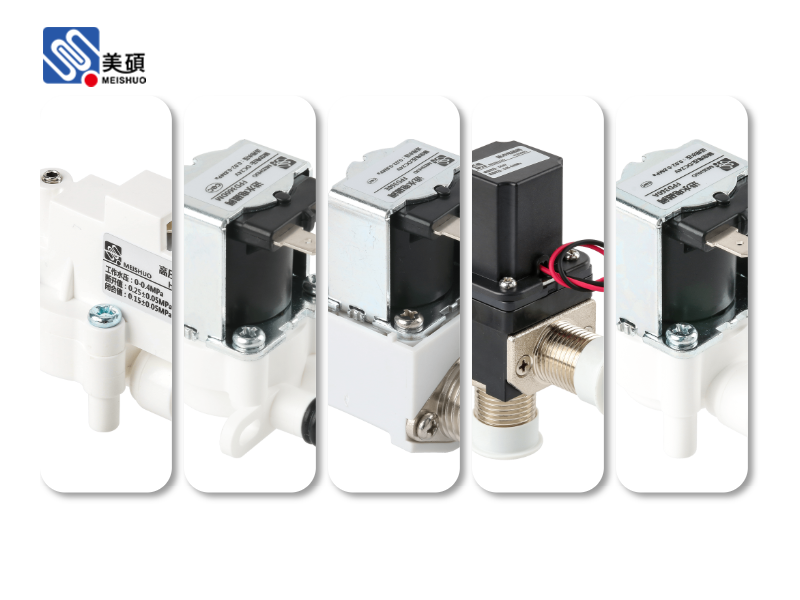
The food grade solenoid valve is a crucial piece of equipment used in various applications within the food and beverage industry. These valves are designed to control the flow of fluids, such as water, air, and gases, in a safe and hygienic manner. To ensure that these valves meet the stringent requirements of the industry, they must undergo food grade solenoid valve certification.
**The Significance of Food Grade Solenoid Valve Certification**
Food grade solenoid valve certification is a process that verifies the compliance of these valves with specific industry standards. This certification process is essential for several reasons:
1. **Safety**: Certified valves are designed to minimize the risk of contamination, ensuring the safety of the end product. 2. **Quality**: Certification ensures that the valves meet the required quality standards, providing reliable performance. 3. **Regulatory Compliance**: Many countries have regulations that require food-grade equipment to be certified, ensuring compliance with these laws. 4. **Consumer Trust**: Certified valves contribute to building consumer trust in the quality and safety of food and beverage products.
**Key Factors to Consider When Selecting a Certified Food Grade Solenoid Valve**
When selecting a food grade solenoid valve, it is crucial to consider the following factors:
1. **Material**: The material used in the valve should be food-grade and resistant to corrosion, ensuring long-term durability and safety. 2. **Design**: The valve's design should be suitable for the specific application, with features such as easy cleaning and maintenance. 3. **Certification**: Ensure that the valve has been certified by a recognized authority, such as the 3A Sanitary Standards or the NSF International. 4. **Performance**: The valve should provide reliable performance, with minimal leakage and consistent operation. 5. **Warranty**: A reputable manufacturer will offer a warranty on their certified valves, providing peace of mind to the end-user.
**Conclusion**
In conclusion, food grade solenoid valve certification is a critical aspect of the food and beverage industry. By selecting certified valves, businesses can ensure the safety, quality, and compliance of their products. As the industry continues to evolve, it is essential to stay informed about the latest developments in food grade solenoid valve certification to maintain the highest standards of operation.
 Chat Oline