In the modern food processing industry, the use of high-quality components is paramount to ensure the safety and quality of the end product. One such critical component is the food grade solenoid valve. This article delves into the significance of food grade solenoid valves in the food industry, their features, and why they are indispensable in maintaining food safety standards.
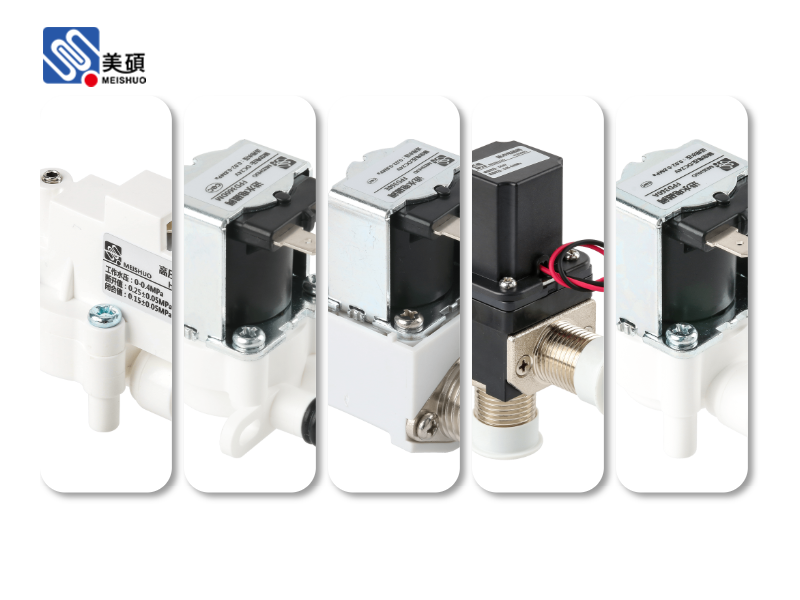
The food grade solenoid valve is a specialized device designed to control the flow of fluids in food processing systems. These valves are specifically engineered to meet the stringent requirements of the food industry, ensuring that they do not contaminate the product or the environment. Their importance in the food processing industry cannot be overstated.
**Features of Food Grade Solenoid Valves**
1. **Material Compatibility**: Food grade solenoid valves are made from materials that are safe for use in food and beverage applications. These materials include stainless steel, polypropylene, and other food-grade plastics. The use of these materials ensures that the valves do not leach harmful substances into the product.
2. **Seal Design**: The seal design of food grade solenoid valves is crucial in preventing any contamination. These valves use FDA-approved seals that are resistant to chemicals and temperature variations, ensuring long-lasting performance.
3. **Easy Cleaning and Sanitization**: The design of food grade solenoid valves facilitates easy cleaning and sanitization. The valves are designed with smooth surfaces and no crevices where bacteria can harbor, making them ideal for use in clean-in-place (CIP) systems.
4. **Sanitary Connections**: Food grade solenoid valves are available with various types of sanitary connections, such as tri-clamp, clamp, and flange, to ensure a secure and leak-proof connection with other equipment.
**Applications of Food Grade Solenoid Valves**
Food grade solenoid valves find extensive use in various applications within the food processing industry, including:
1. **Pumping Systems**: These valves are used to control the flow of liquids, such as water, juice, and sauces, in pumping systems.
2. **Filling Machines**: Food grade solenoid valves are essential in filling machines, where they control the flow of liquids into containers.
3. **CIP Systems**: Clean-in-place systems use food grade solenoid valves to control the flow of cleaning solutions and sanitizing agents.
4. **Cooling and Heating Systems**: These valves are used in cooling and heating systems to control the flow of fluids, such as water and oil, for temperature control.
**Benefits of Using Food Grade Solenoid Valves**
The use of food grade solenoid valves in the food processing industry offers several benefits, including:
1. **Enhanced Food Safety**: These valves help in maintaining food safety standards by preventing contamination and ensuring the quality of the end product.
2. **Cost-Effective**: The use of high-quality components like food grade solenoid valves can lead to reduced maintenance costs and longer equipment lifespan.
3. **Increased Efficiency**: These valves offer precise control over fluid flow, leading to increased efficiency in food processing operations.
4. **Regulatory Compliance**: The use of food grade solenoid valves helps food processing companies comply with regulatory standards and guidelines.
In conclusion, food grade solenoid valves play a crucial role in the food processing industry. Their unique features and benefits make them an indispensable component in ensuring the safety, quality, and efficiency of food processing operations. As the food industry continues to evolve, the demand for high-quality components like food grade solenoid valves is only expected to grow.
 Chat Oline