In the fast-paced world of food processing, the efficiency and safety of operations are paramount. One crucial component that plays a pivotal role in ensuring both these aspects is the food grade solenoid valve. This article delves into the significance of food grade solenoid valves in modern food processing, their types, applications, and benefits.
**Introduction**
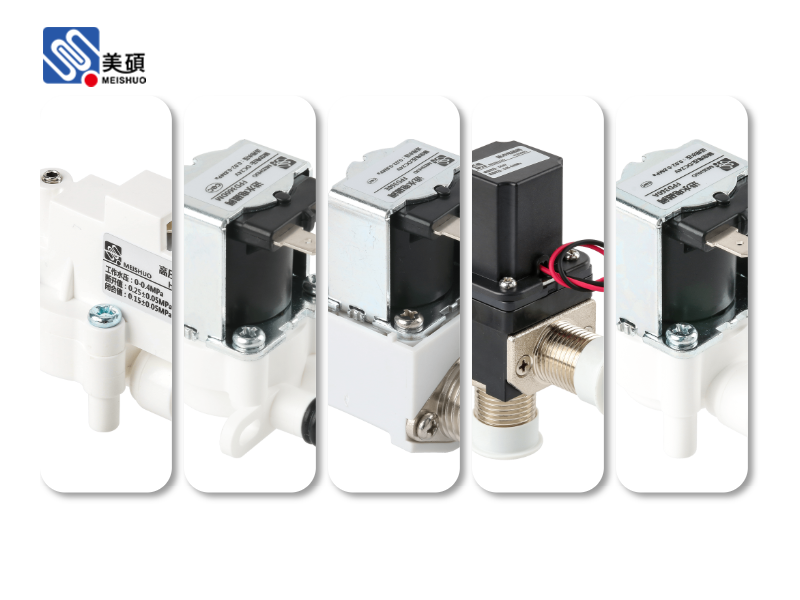
The food industry is one of the most stringent sectors when it comes to safety and quality standards. As such, the equipment used in food processing plants must meet specific criteria to ensure the safety and quality of the end products. Among these critical components, food grade solenoid valves stand out for their unique design and functionality. These valves are specifically designed to handle food-grade fluids, making them an essential part of modern food processing facilities.
**Types of Food Grade Solenoid Valves**
Food grade solenoid valves come in various types, each tailored to specific applications within the food industry. Some of the most common types include:
1. **Pilot Operated Solenoid Valves**: These valves are used in applications where a high flow rate is required. They use a pilot valve to control the main valve, allowing for efficient fluid handling.
2. **Direct Acting Solenoid Valves**: These valves are simple and reliable, making them ideal for applications with low to medium flow rates. They operate directly without the need for a pilot valve.
3. **Three-Way Solenoid Valves**: These valves are used to control the direction of fluid flow. They can be used to switch between two positions or to divert fluid flow to different outlets.
4. **Four-Way Solenoid Valves**: These valves are more complex than three-way valves and can control the direction of fluid flow to four different outlets.
**Applications of Food Grade Solenoid Valves**
Food grade solenoid valves find applications in various areas of the food industry, including:
1. **Beverage Industry**: These valves are used in bottling plants to control the flow of liquids into bottles and to fill them with the desired amount of liquid.
2. **Dairy Industry**: In dairy processing plants, food grade solenoid valves are used to control the flow of milk and other dairy products during pasteurization, packaging, and bottling processes.
3. **Meat Processing Industry**: These valves are used to control the flow of water, brine, and other fluids during the processing of meat products.
4. **Bakery Industry**: In bakery plants, food grade solenoid valves are used to control the flow of ingredients during mixing, baking, and cooling processes.
**Benefits of Food Grade Solenoid Valves**
There are several benefits of using food grade solenoid valves in food processing:
1. **Hygiene**: These valves are designed to prevent contamination, ensuring the safety and quality of the end products.
2. **Efficiency**: Food grade solenoid valves provide precise control over fluid flow, leading to efficient operations and reduced waste.
3. **Durability**: These valves are made from high-quality materials, making them durable and long-lasting.
4. **Ease of Maintenance**: Food grade solenoid valves are easy to clean and maintain, reducing downtime and improving overall efficiency.
**Conclusion**
In conclusion, food grade solenoid valves are an essential component in modern food processing facilities. Their unique design and functionality make them ideal for handling food-grade fluids, ensuring the safety and quality of the end products. As the food industry continues to evolve, the role of food grade solenoid valves is likely to become even more crucial in ensuring efficient and safe operations.
 Chat Oline