In the food processing industry, the quality and safety of products are paramount. One critical component that plays a vital role in ensuring these standards is the food grade solenoid valve. These valves are designed to withstand harsh conditions and maintain the integrity of food products. However, not all solenoid valves are created equal. This article delves into the importance of food grade solenoid valve certification and why it is essential for the food industry.
**Introduction**
The food grade solenoid valve certification is a process that ensures these valves meet specific standards and regulations. These certifications are crucial in maintaining the safety and quality of food products. In this article, we will explore the significance of food grade solenoid valve certification, its benefits, and the key factors that contribute to its effectiveness.
**The Significance of Food Grade Solenoid Valve Certification**
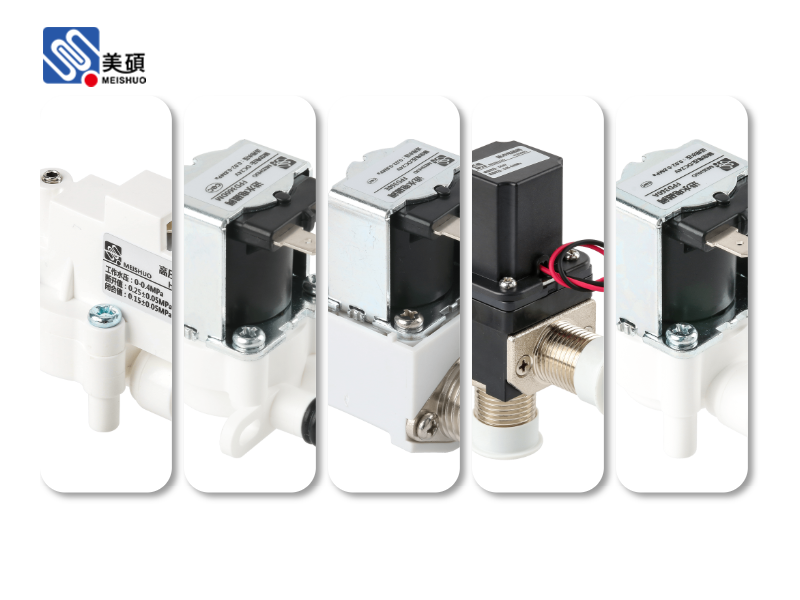
Food grade solenoid valves are used in various applications within the food industry, such as in packaging machines, processing lines, and storage facilities. These valves are responsible for controlling the flow of liquids, gases, and other substances. As such, their performance and reliability are of utmost importance.
The certification process ensures that these valves are designed, manufactured, and tested to meet specific standards. This includes materials used, construction, and performance criteria. By adhering to these standards, food grade solenoid valves can prevent contamination and maintain the quality of food products.
**Benefits of Food Grade Solenoid Valve Certification**
1. **Enhanced Food Safety**: The primary benefit of food grade solenoid valve certification is the enhancement of food safety. These valves are designed to prevent contamination, ensuring that food products remain safe for consumption.
2. **Increased Reliability**: Certified food grade solenoid valves are more reliable than non-certified ones. This is because they are subjected to rigorous testing to ensure they can withstand harsh conditions and maintain performance over time.
3. **Compliance with Regulations**: The food industry is subject to numerous regulations and standards. Food grade solenoid valve certification helps businesses ensure compliance with these regulations, reducing the risk of fines and legal issues.
4. **Improved Product Quality**: By using certified food grade solenoid valves, businesses can improve the quality of their food products. This is because these valves are designed to maintain the integrity of the product throughout the manufacturing process.
**Key Factors Contributing to Food Grade Solenoid Valve Certification**
1. **Material Selection**: The materials used in the construction of food grade solenoid valves must be non-toxic and resistant to corrosion. Common materials include stainless steel, polypropylene, and PTFE.
2. **Design and Construction**: Certified valves must be designed and constructed to withstand harsh conditions and maintain performance over time. This includes factors such as tight tolerances, smooth surfaces, and proper sealing.
3. **Testing and Inspection**: Food grade solenoid valves must undergo rigorous testing and inspection to ensure they meet the required standards. This includes leak tests, pressure tests, and material analysis.
4. **Certification Bodies**: Certification is provided by recognized bodies that are authorized to assess and certify the compliance of food grade solenoid valves with the relevant standards.
**Conclusion**
Food grade solenoid valve certification is a crucial process that ensures the safety and quality of food products. By adhering to specific standards and regulations, these valves can prevent contamination and maintain the integrity of food products throughout the manufacturing process. As the food industry continues to evolve, the importance of food grade solenoid valve certification will only grow, ensuring that consumers can trust the quality and safety of the food they consume.
 Chat Oline