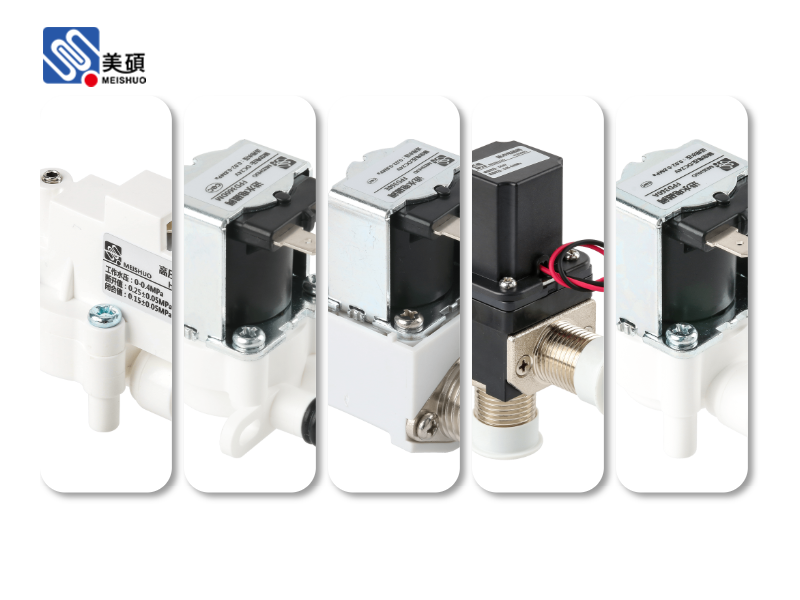
In the highly regulated and meticulous world of food processing, the selection of equipment is critical to ensure safety, efficiency, and compliance with stringent hygiene standards. One such essential component is the Food Grade Solenoid Valve. This article delves into the significance of Food Grade Solenoid Valves in modern food processing, their features, and how they contribute to the overall quality and safety of food products.
The food industry operates under strict regulations to maintain the highest standards of food safety and quality. Food Grade Solenoid Valves are specifically designed to meet these stringent requirements, ensuring that they are safe for use in food and beverage processing environments. These valves are constructed from materials that are non-toxic, corrosion-resistant, and easy to clean, making them ideal for use in the food industry.
One of the primary functions of Food Grade Solenoid Valves is to control the flow of liquids and gases in food processing systems. They are commonly used in applications such as water supply, sanitation, and the conveyance of food products. The precise control offered by these valves is crucial in maintaining the quality and safety of food products.
Food Grade Solenoid Valves are available in various types, including diaphragm, ball, and butterfly valves. Each type has its own unique advantages and is suitable for different applications within the food industry. For instance, diaphragm valves are ideal for use in applications where a tight shut-off is required, while ball valves are well-suited for high-pressure applications.
One of the key features of Food Grade Solenoid Valves is their ability to withstand harsh cleaning and sanitizing processes. This is essential in the food industry, where equipment must be cleaned and sanitized regularly to prevent contamination. These valves are designed to be resistant to chemicals, high temperatures, and aggressive cleaning agents, ensuring that they remain functional and reliable throughout their lifespan.
In addition to their durability and resistance to harsh conditions, Food Grade Solenoid Valves offer several other advantages that make them an essential component in modern food processing. Some of these advantages include:
1. Quick and easy installation: Food Grade Solenoid Valves are designed for quick and easy installation, reducing downtime and labor costs. 2. Energy-efficient: These valves are designed to minimize energy consumption, contributing to a more sustainable and cost-effective operation. 3. Reliable performance: Food Grade Solenoid Valves are known for their reliable performance, ensuring consistent and accurate control of fluid flow. 4. Customizable: These valves can be customized to meet specific requirements, making them suitable for a wide range of applications within the food industry.
The use of Food Grade Solenoid Valves in the food industry has several benefits, including:
1. Improved food safety: By ensuring that the valves are made from safe materials and can withstand harsh cleaning and sanitizing processes, Food Grade Solenoid Valves contribute to the overall safety of food products. 2. Enhanced product quality: The precise control offered by these valves helps maintain the quality of food products, ensuring that they meet the required standards. 3. Increased efficiency: Food Grade Solenoid Valves contribute to a more efficient operation, reducing downtime and labor costs. 4. Compliance with regulations: By using Food Grade Solenoid Valves, food processing facilities can ensure compliance with the strict regulations governing the industry.
In conclusion, Food Grade Solenoid Valves play a crucial role in modern food processing. Their ability to control fluid flow, withstand harsh conditions, and meet stringent hygiene standards makes them an essential component in the food industry. As the demand for safe and high-quality food continues to grow, the importance of Food Grade Solenoid Valves will only increase.
 Chat Oline