In the highly regulated food industry, maintaining safety and compliance is paramount. One crucial component that plays a vital role in ensuring food safety is the food grade solenoid valve. This article delves into the importance of food grade solenoid valve certification and how it ensures safety and compliance in the food industry.
**Introduction**
The food industry operates under strict regulations to ensure that the products consumed by consumers are safe and hygienic. One of the critical components in this process is the solenoid valve, which is used to control the flow of liquids and gases in various food processing systems. Food grade solenoid valves are specifically designed to meet the stringent requirements of the food industry, and their certification is a testament to their compliance with these standards.
**What is a Food Grade Solenoid Valve?**
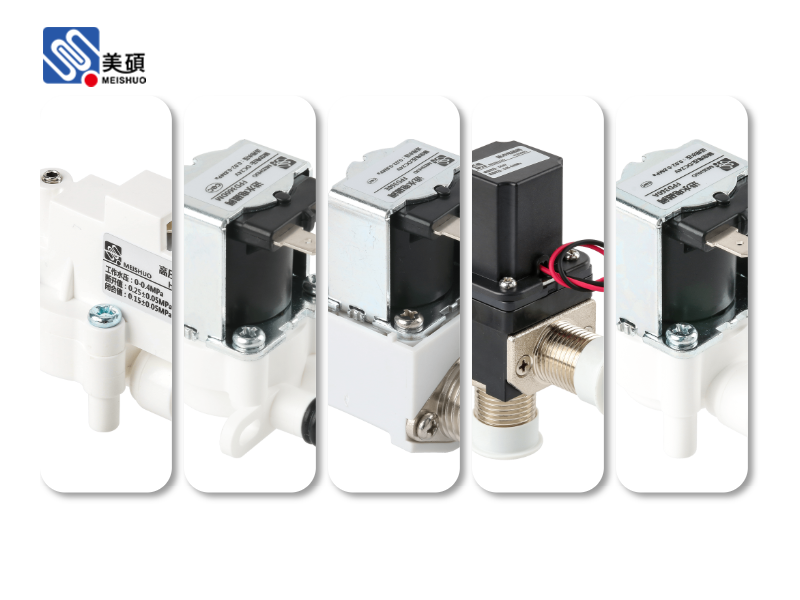
A food grade solenoid valve is a type of valve that is designed for use in food and beverage processing systems. These valves are made from materials that are non-toxic, corrosion-resistant, and easy to clean. They are also designed to prevent the buildup of bacteria and other contaminants, ensuring that the food products remain safe and uncontaminated.
**The Importance of Food Grade Solenoid Valve Certification**
Food grade solenoid valve certification is a process that ensures that these valves meet the necessary standards for use in the food industry. Certification is typically carried out by independent third-party organizations that specialize in testing and certifying products for use in the food industry.
There are several reasons why food grade solenoid valve certification is important:
1. **Safety**: Certification ensures that the valves are safe for use in food processing systems, reducing the risk of contamination and ensuring the safety of the end product. 2. **Compliance**: Certification helps manufacturers and users of food grade solenoid valves to comply with the regulations and standards set by regulatory bodies, such as the FDA and the EU. 3. **Quality Assurance**: Certification provides a level of quality assurance, ensuring that the valves meet the necessary standards for use in the food industry. 4. **Trust and Credibility**: Certification helps to build trust and credibility among consumers, as they can be confident that the products they are purchasing are safe and compliant with industry standards.
**The Certification Process**
The certification process for food grade solenoid valves typically involves several steps:
1. **Material Testing**: The materials used in the construction of the valve are tested to ensure that they meet the necessary standards for use in the food industry. 2. **Performance Testing**: The valve is tested to ensure that it operates as expected and meets the necessary performance criteria. 3. **Hygiene Testing**: The valve is tested to ensure that it is easy to clean and sanitize, reducing the risk of contamination. 4. **Documentation**: The manufacturer must provide detailed documentation that proves that the valve meets the necessary standards.
**Conclusion**
Food grade solenoid valve certification is a critical component of ensuring safety and compliance in the food industry. By choosing certified valves, manufacturers and users can be confident that they are using products that meet the necessary standards for use in food processing systems. As the food industry continues to evolve, the importance of food grade solenoid valve certification will only grow, ensuring that consumers can trust the safety and quality of the food they consume.
 Chat Oline