The food industry is one of the most critical sectors in the global economy, and ensuring the safety and quality of food products is paramount. In this context, the use of food-grade solenoid valves has become increasingly important. This article explores the role of food-grade solenoid valves in modern food processing, their benefits, and why they are essential for maintaining high-quality food products.
**Introduction**
Food-grade solenoid valves are specialized devices designed for use in food and beverage processing systems. These valves are constructed with materials that meet the stringent requirements of the food industry, ensuring that they do not contaminate the food or beverage products they handle. In this article, we will delve into the various aspects of food-grade solenoid valves, their applications, and the advantages they offer in the food processing industry.
**What is a Food-Grade Solenoid Valve?**
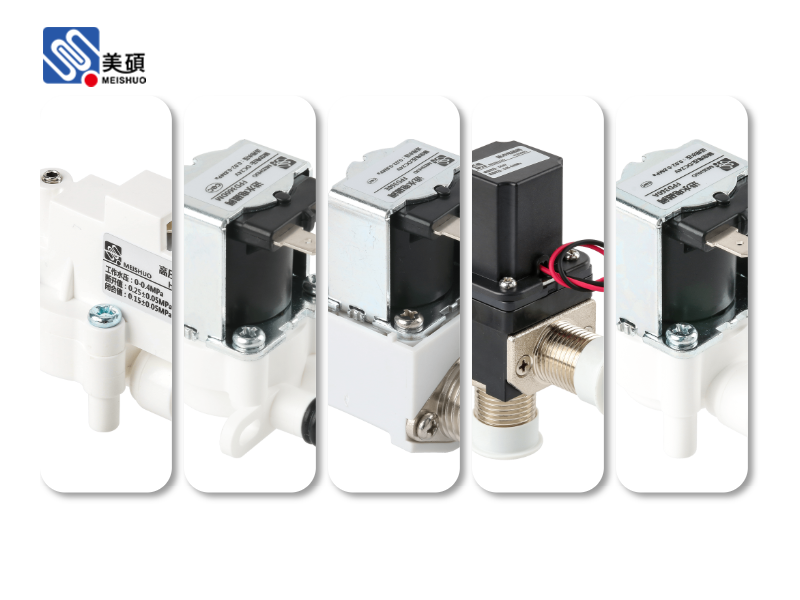
A food-grade solenoid valve is an electromechanical device that controls the flow of fluids in a system. These valves are designed to be used in environments where hygiene and safety are of utmost importance, such as in the food and beverage industry. They are typically made from materials like stainless steel, polypropylene, and PTFE, which are non-toxic and resistant to corrosion.
**Applications of Food-Grade Solenoid Valves in Food Processing**
Food-grade solenoid valves find a wide range of applications in the food processing industry. Some of the most common uses include:
1. **Watering Systems**: Food-grade solenoid valves are used to control the flow of water in irrigation systems, ensuring that plants receive the right amount of water for optimal growth.
2. **Sanitization Systems**: These valves are used in sanitization systems to control the flow of cleaning agents and water, ensuring that equipment is thoroughly cleaned and sanitized.
3. **Dosing Systems**: Food-grade solenoid valves are used in dosing systems to accurately measure and dispense small amounts of ingredients, such as flavorings, colorants, and preservatives.
4. **Packaging Machines**: These valves are used in packaging machines to control the flow of liquids, such as sauces, oils, and condiments, into packaging containers.
**Benefits of Using Food-Grade Solenoid Valves**
There are several benefits to using food-grade solenoid valves in food processing:
1. **Hygiene**: The materials used in food-grade solenoid valves are non-toxic and resistant to corrosion, making them ideal for use in food and beverage processing systems.
2. **Safety**: These valves are designed to prevent contamination of food products, ensuring the safety of consumers.
3. **Precision**: Food-grade solenoid valves offer precise control over the flow of fluids, allowing for accurate dosing and efficient operation.
4. **Durability**: The materials used in these valves are durable and can withstand harsh conditions, such as high temperatures and aggressive chemicals.
**Conclusion**
Food-grade solenoid valves play a crucial role in modern food processing, ensuring the safety, quality, and efficiency of food and beverage production. Their use in various applications, coupled with their numerous benefits, makes them an essential component of the food processing industry. As the demand for high-quality food products continues to grow, the importance of food-grade solenoid valves will only increase.
 Chat Oline