In the food and beverage industry, the safety and quality of products are paramount. One critical component that plays a vital role in ensuring these standards is the food grade solenoid valve. This article delves into the importance of food grade solenoid valve certification, its benefits, and the process involved in obtaining it.
**Introduction**
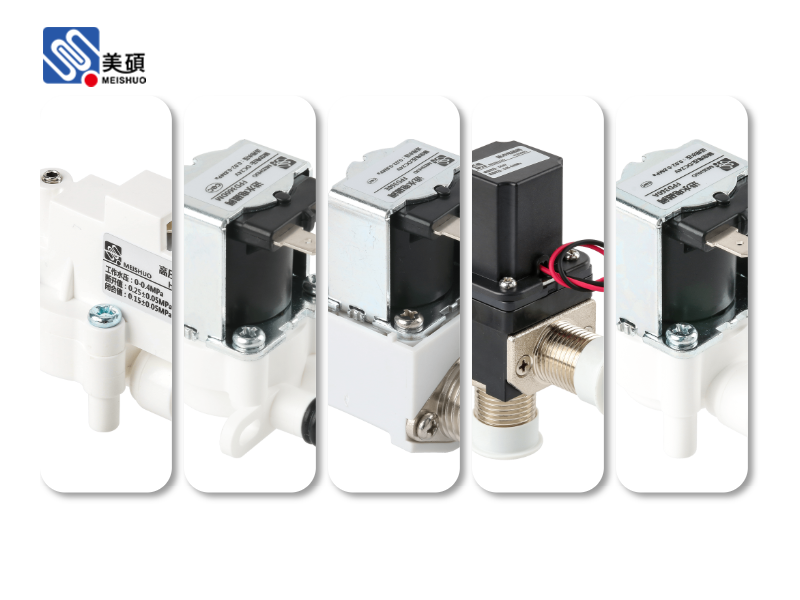
The food grade solenoid valve is a crucial component in many food processing systems. It is designed to control the flow of fluids, such as water, air, and various chemicals, in a safe and hygienic manner. As a result, the certification of these valves is essential to ensure that they meet the stringent requirements of the food industry. This article will explore the significance of food grade solenoid valve certification, its benefits, and the steps involved in obtaining certification.
**The Importance of Food Grade Solenoid Valve Certification**
Food grade solenoid valves are subject to rigorous testing and certification to ensure they meet the necessary safety and hygiene standards. Certification is essential for several reasons:
1. **Compliance with Regulations**: The food industry is heavily regulated, and the use of certified components is often a legal requirement. Certification ensures that food grade solenoid valves comply with these regulations, reducing the risk of legal issues and fines.
2. **Safety and Hygiene**: Certified valves are designed to prevent contamination and maintain hygiene in food processing systems. This is crucial in preventing the spread of foodborne illnesses and ensuring the safety of consumers.
3. **Quality Assurance**: Certification provides a guarantee that the valves meet the required quality standards. This helps manufacturers and end-users to have confidence in the performance and reliability of the valves.
**Benefits of Food Grade Solenoid Valve Certification**
There are several benefits to obtaining food grade solenoid valve certification:
1. **Improved Marketability**: Certified valves are more likely to be accepted by customers and end-users in the food industry. This can lead to increased sales and market share.
2. **Enhanced Reputation**: Certification demonstrates a company's commitment to quality and safety, enhancing its reputation in the industry.
3. **Reduced Costs**: By ensuring that valves meet the necessary standards, certification can help to avoid costly recalls, fines, and legal issues.
**The Certification Process**
The process of obtaining food grade solenoid valve certification typically involves the following steps:
1. **Selection of a Certification Body**: The first step is to select a certification body that is recognized by relevant authorities. This body will oversee the certification process.
2. **Preparation of Documentation**: The manufacturer must prepare detailed documentation, including technical specifications, design drawings, and quality control procedures.
3. **Factory Audit**: A certification body will conduct a factory audit to ensure that the manufacturing process meets the required standards. This may involve inspecting the manufacturing facilities, equipment, and quality control systems.
4. **Testing**: The valves will be subjected to various tests to assess their performance, durability, and safety. These tests may include pressure testing, material analysis, and hygiene assessments.
5. **Certification Issuance**: Once the audit and testing are complete, the certification body will issue a certificate if the valves meet the required standards.
**Conclusion**
Food grade solenoid valve certification is an essential step in ensuring the safety and quality of products in the food and beverage industry. By obtaining certification, manufacturers can demonstrate their commitment to quality and safety, improve marketability, and reduce costs. As the demand for certified components continues to grow, it is crucial for manufacturers to understand the certification process and its benefits.
 Chat Oline