In the highly regulated and meticulous world of food processing, the use of high-quality components is paramount to ensure safety, efficiency, and compliance with stringent hygiene standards. One such critical component is the Food Grade Solenoid Valve. This article delves into the significance of Food Grade Solenoid Valves in modern food processing, exploring their features, benefits, and applications.
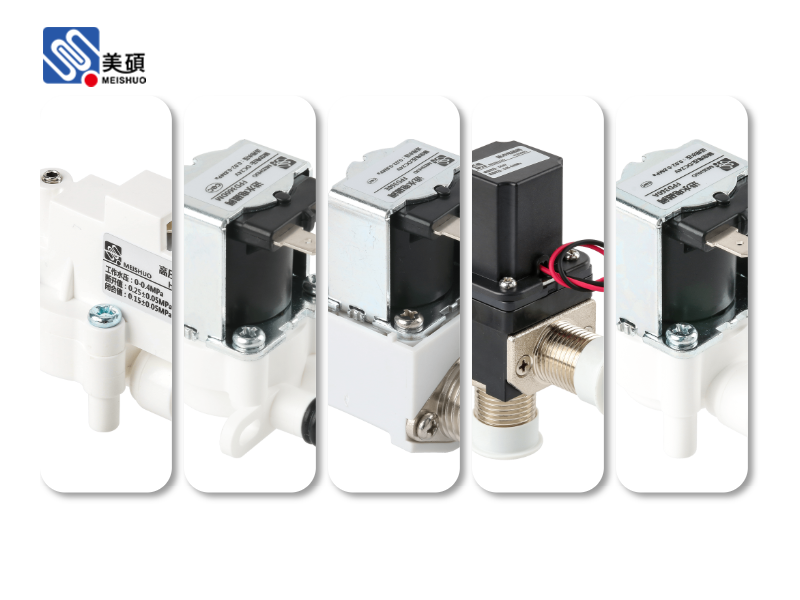
The Food Grade Solenoid Valve: A Brief Overview A Food Grade Solenoid Valve is a type of electromagnetic valve designed for use in food and beverage processing systems. These valves are specifically engineered to meet the stringent requirements of the food industry, including resistance to corrosion, high temperatures, and the ability to handle a wide range of fluids. They are commonly used in applications such as water supply, sanitation, and the control of cleaning agents.
Key Features of Food Grade Solenoid Valves 1. Material Selection: Food Grade Solenoid Valves are constructed using materials that are safe for contact with food and beverages. Common materials include stainless steel, polypropylene, and FDA-approved plastics. 2. Hygienic Design: These valves are designed with smooth surfaces and crevice-free construction to prevent the accumulation of bacteria and other contaminants. 3. Reliable Sealing: Food Grade Solenoid Valves feature robust sealing mechanisms that ensure a tight closure, minimizing the risk of leaks and cross-contamination. 4. Easy Cleaning: The design of these valves allows for easy disassembly and cleaning, making them ideal for use in environments where hygiene is a top priority.
Benefits of Using Food Grade Solenoid Valves 1. Enhanced Safety: By using Food Grade Solenoid Valves, food processing facilities can minimize the risk of contamination, ensuring the safety of consumers. 2. Improved Efficiency: These valves offer precise control over fluid flow, leading to improved process efficiency and reduced downtime. 3. Cost-Effective: Despite their higher initial cost, Food Grade Solenoid Valves can be more cost-effective in the long run due to their durability and reduced maintenance requirements. 4. Compliance with Regulations: The use of Food Grade Solenoid Valves helps food processing facilities comply with industry regulations and standards, such as the FDA and ISO 22000.
Applications of Food Grade Solenoid Valves 1. Water Supply: Food Grade Solenoid Valves are commonly used to control the flow of water in food processing systems, ensuring a constant supply of clean water. 2. Sanitation: These valves play a crucial role in the sanitation process, allowing for the efficient cleaning and disinfection of equipment and facilities. 3. Cleaning Agents: Food Grade Solenoid Valves are used to control the flow of cleaning agents, ensuring that they are applied in the correct concentration and volume. 4. Process Control: These valves are used in various process control applications, such as the regulation of pressure, temperature, and flow rate.
Conclusion The Food Grade Solenoid Valve is an indispensable component in modern food processing. Its unique features, benefits, and applications make it an essential tool for ensuring safety, efficiency, and compliance with industry standards. As the food industry continues to evolve, the demand for high-quality, reliable components like the Food Grade Solenoid Valve will only grow.
 Chat Oline