In today's environmentally conscious world, the demand for RoHS compliant products has never been higher. One such product that stands out is the RoHS compliant solenoid valve. This article aims to provide a comprehensive guide to understanding what RoHS compliant solenoid valves are, their benefits, and how they are used across various industries.
**Introduction**
The RoHS Directive, which stands for the Restriction of Hazardous Substances, is a European Union regulation that restricts the use of certain hazardous materials in electrical and electronic equipment. The main goal of RoHS is to protect human health and the environment from the potential hazards of these substances. One of the key components affected by this directive is the solenoid valve, which is widely used in various industries.
**What is a RoHS Compliant Solenoid Valve?**
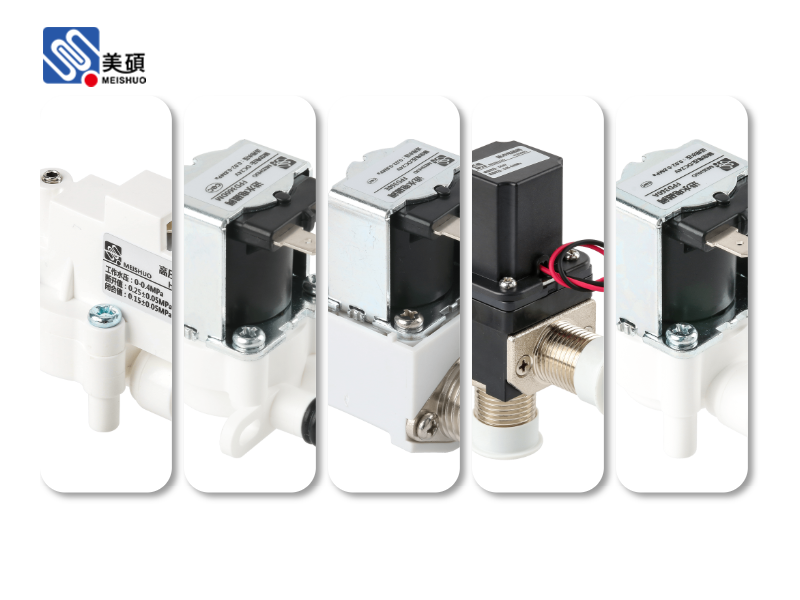
A RoHS compliant solenoid valve is a type of valve that meets the requirements set forth by the RoHS Directive. This means that it contains no more than the maximum allowable concentrations of the restricted substances, such as lead, cadmium, mercury, hexavalent chromium, polybrominated biphenyls (PBBs), and polybrominated diphenyl ethers (PBDEs).
**Benefits of Using RoHS Compliant Solenoid Valves**
1. **Environmental Protection**: By using RoHS compliant solenoid valves, manufacturers can reduce the environmental impact of their products, contributing to a greener and more sustainable future.
2. **Market Access**: Many countries, including the European Union, require RoHS compliance for products sold within their borders. By using RoHS compliant solenoid valves, manufacturers can ensure that their products meet these requirements and gain access to a wider market.
3. **Consumer Confidence**: Consumers are increasingly aware of environmental issues and prefer to purchase products that are environmentally friendly. Using RoHS compliant solenoid valves can help manufacturers build trust with their customers.
4. **Regulatory Compliance**: Compliance with the RoHS Directive is not only a legal requirement but also a sign of a company's commitment to ethical and sustainable business practices.
**Applications of RoHS Compliant Solenoid Valves**
RoHS compliant solenoid valves are used in a wide range of industries, including:
1. **Automotive Industry**: Solenoid valves are used in vehicles for various applications, such as fuel injection systems, brake systems, and air conditioning systems.
2. **Pharmaceutical Industry**: Solenoid valves are used in pharmaceutical manufacturing processes for controlling the flow of liquids and gases.
3. **Food and Beverage Industry**: Solenoid valves are used in food processing and packaging facilities for controlling the flow of liquids and gases.
4. **Industrial Automation**: Solenoid valves are used in industrial automation systems for controlling the flow of fluids and gases in various processes.
**Conclusion**
In conclusion, the RoHS compliant solenoid valve is an essential component in today's environmentally conscious world. By choosing RoHS compliant solenoid valves, manufacturers can not only ensure regulatory compliance but also contribute to a healthier environment and a more sustainable future.
 Chat Oline