The food industry is a highly regulated sector, demanding precision, safety, and efficiency in every aspect of production. One critical component that plays a pivotal role in ensuring the quality and safety of food products is the food grade solenoid valve. This article delves into the significance of food grade solenoid valves, their working principles, and the benefits they offer to the food industry.
**Introduction**
In the food industry, where hygiene and safety are paramount, the use of high-quality components is essential. Food grade solenoid valves are specifically designed to meet the stringent requirements of the food processing industry. These valves are used in various applications, including the control of liquid and gas flow in food and beverage processing systems, ensuring that the end product is safe for consumption.
**What is a Food Grade Solenoid Valve?**
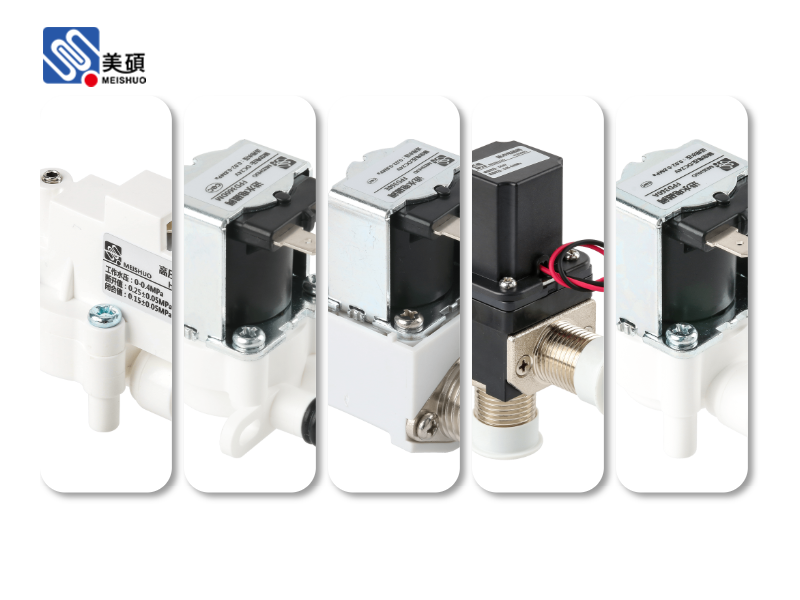
A food grade solenoid valve is a type of electromagnetic valve that controls the flow of fluids in a system. Unlike conventional solenoid valves, food grade valves are made from materials that are safe for use in food and beverage processing environments. These materials are non-toxic, corrosion-resistant, and easy to clean, making them ideal for use in the food industry.
**Working Principles of Food Grade Solenoid Valves**
Food grade solenoid valves operate on the principle of electromagnetic induction. When an electric current passes through the coil, it creates a magnetic field that attracts a plunger, which in turn opens or closes the valve. This process is quick and efficient, allowing for precise control of fluid flow.
**Benefits of Food Grade Solenoid Valves in the Food Industry**
1. **Hygiene and Safety**: Food grade solenoid valves are made from materials that are safe for use in food processing environments. This ensures that there is no risk of contamination or harmful substances entering the food supply chain.
2. **Durability**: These valves are designed to withstand harsh conditions, including high temperatures, pressure, and aggressive chemicals. This durability ensures that they can last for many years, reducing maintenance costs and downtime.
3. **Precision and Control**: Food grade solenoid valves offer precise control over fluid flow, which is crucial in the food industry. This precision ensures that the end product meets the required quality standards.
4. **Ease of Cleaning**: The materials used in food grade solenoid valves are easy to clean, which is essential in maintaining hygiene in food processing facilities. This also reduces the risk of cross-contamination between different products.
5. **Energy Efficiency**: These valves are designed to be energy-efficient, which helps to reduce operating costs and minimize the environmental impact of food processing operations.
**Applications of Food Grade Solenoid Valves**
Food grade solenoid valves are used in a wide range of applications in the food industry, including:
- **Watering systems**: For controlling the flow of water in irrigation systems. - **Dairy processing**: For controlling the flow of milk and other dairy products. - **Beverage production**: For controlling the flow of liquids in bottling and packaging processes. - **Baking and confectionery**: For controlling the flow of ingredients and liquids in mixing and processing equipment.
**Conclusion**
Food grade solenoid valves are an essential component in the food industry, providing precision, safety, and efficiency in fluid control. With their numerous benefits and wide range of applications, these valves play a crucial role in ensuring the quality and safety of food products. As the food industry continues to evolve, the demand for high-quality, reliable components like food grade solenoid valves will only increase.
 Chat Oline