The food industry is one of the most stringent sectors when it comes to the quality and safety of its products. As such, the equipment used in food processing must meet high standards of hygiene and efficiency. One such essential component is the food grade solenoid valve. This article delves into the world of food grade solenoid valves, exploring their significance, types, and applications in the modern food processing industry.
Introducing the Food Grade Solenoid Valve
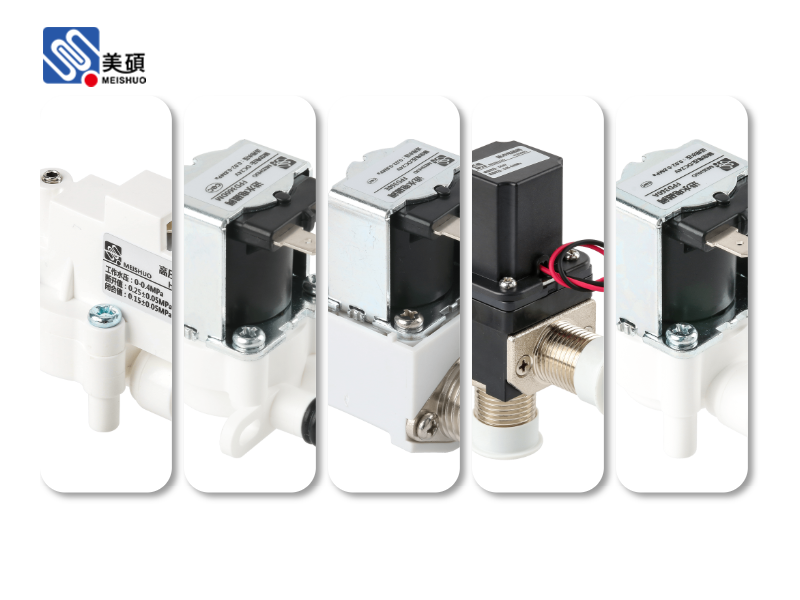
A solenoid valve is a type of valve that uses an electromagnetic coil to open or close a valve body. Food grade solenoid valves are specifically designed to handle food-grade applications, ensuring that they meet the stringent hygiene requirements of the food industry. These valves are made from materials that are non-toxic, corrosion-resistant, and easy to clean.
Types of Food Grade Solenoid Valves
1. Direct Acting Solenoid Valves: These valves are simple and reliable, with a direct relationship between the coil current and the valve stroke. They are commonly used in applications with low pressure and flow rates.
2. Pilot Operated Solenoid Valves: These valves offer better control over the flow rate and pressure drop. They use a pilot valve to control the main valve, allowing for precise regulation of the fluid flow.
3. Double Acting Solenoid Valves: These valves have two coils, one for opening and the other for closing. They are suitable for applications that require frequent and rapid changes in direction or position.
Applications of Food Grade Solenoid Valves in the Food Industry
1. Beverage Industry: Food grade solenoid valves are extensively used in the beverage industry for controlling the flow of liquids, such as water, juice, and beer. They help maintain the quality and safety of the products by preventing contamination and ensuring consistent flow rates.
2. Dairy Industry: These valves are used for controlling the flow of milk, cream, and other dairy products. They are crucial in maintaining the quality and safety of dairy products by preventing bacterial growth and ensuring hygienic conditions.
3. Meat Processing Industry: Food grade solenoid valves are used for controlling the flow of water, brine, and other fluids in meat processing plants. They help maintain the quality and safety of meat products by ensuring hygienic conditions and preventing cross-contamination.
4. Bakery Industry: These valves are used for controlling the flow of ingredients, such as flour, sugar, and water, in bakery plants. They help maintain the quality and consistency of bakery products by ensuring accurate and consistent ingredient ratios.
Advantages of Food Grade Solenoid Valves
1. Hygiene: Food grade solenoid valves are made from materials that are non-toxic and corrosion-resistant, ensuring that they meet the stringent hygiene requirements of the food industry.
2. Reliability: These valves are designed to be durable and reliable, with long lifespans and minimal maintenance requirements.
3. Flexibility: Food grade solenoid valves come in various types and sizes, making them suitable for a wide range of applications in the food industry.
4. Energy Efficiency: These valves are designed to be energy-efficient, reducing energy consumption and costs for food processing plants.
Conclusion
Food grade solenoid valves play a crucial role in ensuring the quality, safety, and efficiency of food processing operations. Their versatility, reliability, and hygiene make them an essential component in the modern food industry. As the industry continues to evolve, the demand for high-quality, food-grade solenoid valves is expected to grow, making them an indispensable part of the food processing landscape.
 Chat Oline