In today's environmentally conscious world, the demand for RoHS compliant products has never been higher. One such product that stands out in the industrial sector is the RoHS compliant solenoid valve. This article delves into the significance of RoHS compliance, the benefits of using RoHS compliant solenoid valves, and how they contribute to sustainable and efficient operations.
The RoHS Directive, or Restriction of Hazardous Substances, is a European Union regulation that restricts the use of certain hazardous substances in electrical and electronic equipment. These substances include lead, mercury, cadmium, hexavalent chromium, polybrominated biphenyls, and polybrominated diphenyl ethers. The primary aim of the RoHS Directive is to protect human health and the environment from the potential hazards posed by these substances.
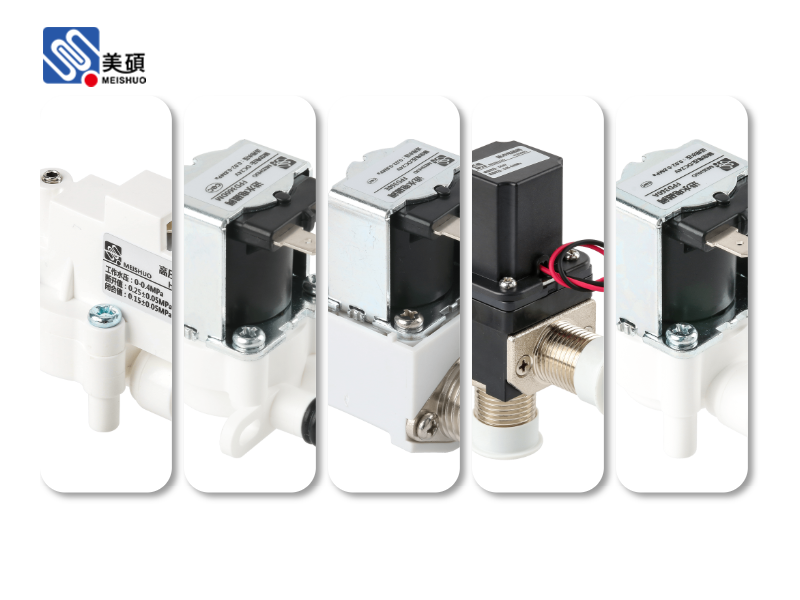
RoHS compliant solenoid valves are designed to meet the stringent requirements of the RoHS Directive. They are engineered without the use of restricted substances, ensuring that they are environmentally friendly and safe for human health. This makes them an ideal choice for industries that prioritize sustainability and compliance with regulatory standards.
One of the key benefits of using RoHS compliant solenoid valves is their reliability. These valves are built to withstand harsh operating conditions, making them suitable for a wide range of applications, from industrial processes to automotive systems. Their robust construction and high-quality materials ensure long-lasting performance, reducing the need for frequent replacements and maintenance.
Another advantage of RoHS compliant solenoid valves is their energy efficiency. These valves are designed to minimize energy consumption, which not only helps in reducing operational costs but also contributes to a greener environment. By choosing RoHS compliant solenoid valves, businesses can align their operations with global sustainability goals and demonstrate their commitment to environmental responsibility.
In addition to environmental benefits, RoHS compliant solenoid valves offer several practical advantages. They are available in a wide range of configurations, including different sizes, pressures, and flow rates, allowing engineers to select the perfect valve for their specific application. This flexibility makes them a versatile solution for various industries, such as pharmaceuticals, food processing, and water treatment.
The manufacturing process of RoHS compliant solenoid valves is also worth mentioning. These valves are produced using advanced techniques and quality control measures to ensure that they meet the highest standards of performance and reliability. This attention to detail not only guarantees the longevity of the valves but also ensures that they are free from defects and malfunctions.
In conclusion, RoHS compliant solenoid valves are a smart choice for businesses looking to maximize efficiency while adhering to environmental regulations. Their reliability, energy efficiency, and versatility make them an invaluable asset in a wide range of applications. By choosing RoHS compliant solenoid valves, companies can not only contribute to a healthier planet but also enhance their operational performance and reduce costs in the long run.
 Chat Oline