In the food and beverage industry, ensuring the highest standards of quality and safety is paramount. One critical component that plays a pivotal role in maintaining these standards is the food grade solenoid valve. This article delves into the importance of food grade solenoid valve certification, the process involved, and the benefits it brings to the industry.
**Introduction**
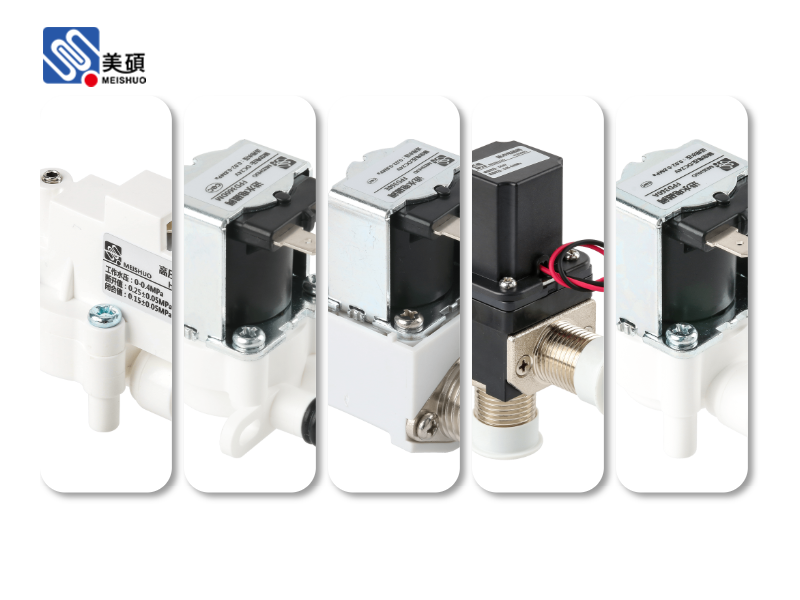
The food grade solenoid valve is a crucial piece of equipment used in various applications within the food and beverage industry. These valves are designed to control the flow of fluids, such as water, air, and other gases, in a safe and hygienic manner. To ensure that these valves meet the stringent requirements of the industry, they must undergo food grade solenoid valve certification.
**Understanding Food Grade Solenoid Valve Certification**
Food grade solenoid valve certification is a process that verifies whether a valve meets the necessary standards for use in the food and beverage industry. These standards are set by regulatory bodies and industry associations to ensure that the valves are safe, reliable, and hygienic.
The certification process typically involves several steps:
1. **Material Selection**: The materials used in the construction of food grade solenoid valves must be safe for contact with food. This includes materials such as stainless steel, polypropylene, and other food-grade materials.
2. **Design and Construction**: The design and construction of food grade solenoid valves must be such that they do not contaminate the food or beverage being processed. This includes features such as smooth interiors, no sharp edges, and easy-to-clean surfaces.
3. **Testing and Inspection**: Food grade solenoid valves must undergo rigorous testing and inspection to ensure they meet the required standards. This includes tests for pressure, temperature, and material compatibility.
4. **Certification**: Once a valve has passed all the necessary tests and inspections, it is awarded a certification. This certification serves as proof that the valve meets the required standards and is safe for use in the food and beverage industry.
**Benefits of Food Grade Solenoid Valve Certification**
The food grade solenoid valve certification process offers several benefits to the industry:
1. **Enhanced Safety**: By ensuring that food grade solenoid valves meet the necessary standards, the certification process helps to reduce the risk of contamination and improve food safety.
2. **Increased Reliability**: Certified valves are more likely to be reliable and long-lasting, reducing downtime and maintenance costs.
3. **Improved Hygiene**: The design and construction of food grade solenoid valves are optimized for easy cleaning and maintenance, which helps to maintain a high level of hygiene in food processing facilities.
4. **Compliance with Regulations**: Certification ensures that food grade solenoid valves comply with the relevant regulations and standards, which is crucial for businesses operating in the food and beverage industry.
**Conclusion**
Food grade solenoid valve certification is an essential process for ensuring the safety, reliability, and hygiene of valves used in the food and beverage industry. By adhering to the strict standards set by regulatory bodies and industry associations, food grade solenoid valves provide peace of mind to businesses and consumers alike.
 Chat Oline