In the highly regulated and demanding food industry, the use of food grade solenoid valves is essential for ensuring product safety and quality. These specialized valves play a crucial role in the processing and handling of food products, providing precise control over the flow of fluids. This article delves into the significance of food grade solenoid valves in modern food processing, exploring their features, applications, and advantages.
The Importance of Food Grade Solenoid Valves
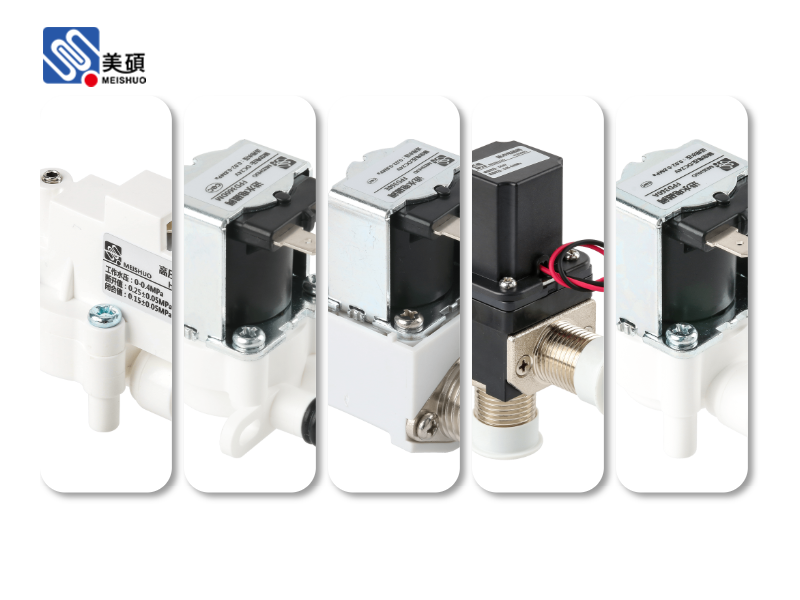
Food grade solenoid valves are specifically designed to meet the stringent requirements of the food industry. Unlike standard solenoid valves, these valves are constructed with materials that are non-toxic, corrosion-resistant, and easy to clean. This ensures that they do not contaminate food products and maintain the highest level of hygiene.
Features of Food Grade Solenoid Valves
One of the key features of food grade solenoid valves is their robust construction. These valves are typically made from materials such as stainless steel, polypropylene, or PTFE, which are known for their durability and resistance to chemicals and heat. This makes them ideal for use in harsh environments found in food processing plants.
Another important feature is the tight sealing capabilities of food grade solenoid valves. They are designed to prevent any leakage, ensuring that food products remain uncontaminated and safe for consumption. This is particularly important in the handling of sensitive products such as baby food or organic foods.
Applications of Food Grade Solenoid Valves
Food grade solenoid valves find widespread applications in various stages of food processing. Some of the most common applications include:
1. Washing and sanitation: Food grade solenoid valves are used to control the flow of water and cleaning agents in washing and sanitation processes, ensuring that equipment and containers are thoroughly cleaned and disinfected. 2. Filling and dispensing: These valves are used to control the flow of liquids during filling and dispensing operations, such as bottling or packaging. They help maintain precise flow rates and minimize product waste. 3. Mixing and blending: Food grade solenoid valves are used to control the flow of ingredients and additives during mixing and blending processes, ensuring consistent product quality and taste. 4. Storage and distribution: These valves are used to control the flow of liquids in storage tanks and pipelines, as well as during distribution to retailers and consumers.
Advantages of Using Food Grade Solenoid Valves
There are several advantages to using food grade solenoid valves in food processing:
1. Improved safety and quality: These valves help ensure the safety and quality of food products by preventing contamination and maintaining consistent processing conditions. 2. Increased efficiency: The precise control provided by food grade solenoid valves can help optimize processing operations, reduce waste, and improve overall efficiency. 3. Cost savings: By minimizing product waste and improving process efficiency, food grade solenoid valves can help reduce operating costs. 4. Compliance with regulations: The use of food grade solenoid valves helps food processors meet the strict regulatory requirements of the industry.
Conclusion
Food grade solenoid valves are an indispensable component in modern food processing. Their specialized design, robust construction, and precise control capabilities make them ideal for use in the food industry. As the demand for safe and high-quality food continues to grow, the role of food grade solenoid valves in ensuring product safety and quality will only become more significant.
 Chat Oline