The food industry is a highly regulated sector, where the quality and safety of products are paramount. One of the critical components that ensure the integrity of food processing and packaging systems is the Food Grade Solenoid Valve. This article delves into the world of Food Grade Solenoid Valves, exploring their significance, features, and applications in the food industry.
**Introduction**
In the food industry, the use of high-quality components is essential to maintain hygiene and prevent contamination. Food Grade Solenoid Valves are specifically designed to meet these stringent requirements. These valves play a crucial role in controlling the flow of liquids, gases, and slurries in various food processing applications. This article aims to provide a comprehensive understanding of Food Grade Solenoid Valves, their benefits, and their applications in the food industry.
**What is a Food Grade Solenoid Valve?**
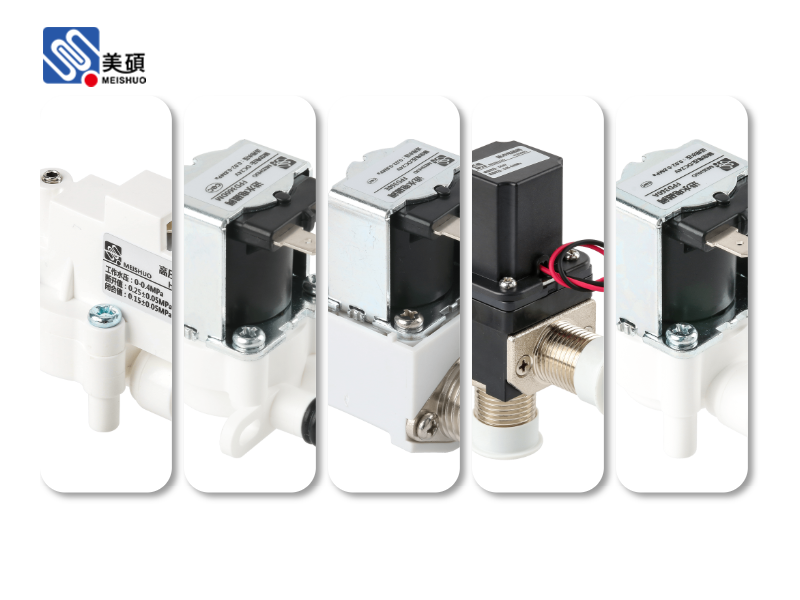
A Food Grade Solenoid Valve is a type of electromagnetic valve that uses an electromagnetic coil to open or close a valve body. These valves are designed to handle food-grade materials, ensuring that they meet the strict hygiene standards required in the food industry. They are commonly used in applications such as washing, sanitizing, and filling processes.
**Key Features of Food Grade Solenoid Valves**
1. **Material Compatibility**: Food Grade Solenoid Valves are made from materials that are safe for contact with food, such as stainless steel, polypropylene, and PTFE. These materials are non-toxic and resistant to corrosion, ensuring the valves do not contaminate the food products.
2. **Hygienic Design**: The design of Food Grade Solenoid Valves is focused on minimizing the risk of contamination. They feature smooth surfaces, crevice-free designs, and easy-to-clean components, making them ideal for use in food processing and packaging systems.
3. **Sanitizable**: These valves can be easily sanitized to remove any potential contaminants. They are designed to withstand high-temperature cleaning processes, ensuring that they remain hygienic at all times.
4. **Reliability**: Food Grade Solenoid Valves are built to last. They are designed with high-quality components and undergo rigorous testing to ensure their reliability and durability.
**Applications of Food Grade Solenoid Valves in the Food Industry**
1. **Washing and Sanitizing**: Food Grade Solenoid Valves are used to control the flow of water and cleaning agents in washing and sanitizing processes. They ensure that the correct amount of cleaning solution is used, optimizing the cleaning process and reducing the risk of contamination.
2. **Filling and Packaging**: These valves are used in filling and packaging machines to control the flow of liquids and gases into containers. They ensure accurate and consistent filling, reducing the risk of overfilling or underfilling.
3. **Process Control**: Food Grade Solenoid Valves are used in process control systems to regulate the flow of materials in various stages of food processing. This helps maintain the quality and consistency of the final product.
**Conclusion**
Food Grade Solenoid Valves are an essential component in the food industry, providing reliable and hygienic control of the flow of liquids, gases, and slurries. Their material compatibility, hygienic design, and sanitizable properties make them ideal for use in food processing and packaging systems. As the food industry continues to evolve, the demand for high-quality, reliable components like Food Grade Solenoid Valves will only increase.
 Chat Oline