In today's world, where environmental concerns are at the forefront, the demand for RoHS compliant products has surged. One such product that has gained significant attention is the RoHS compliant solenoid valve. This article aims to provide a comprehensive guide to understanding what RoHS compliant solenoid valves are, their benefits, and how they are revolutionizing various industries.
**Introduction**
The RoHS directive, or the Restriction of Hazardous Substances, is a European Union regulation that restricts the use of certain hazardous substances in electrical and electronic equipment. These substances include lead, mercury, cadmium, hexavalent chromium, polybrominated biphenyls, and polybrominated diphenyl ethers. The RoHS compliant solenoid valve is designed to meet these stringent regulations, ensuring that the products that use them are environmentally friendly and safe for human health.
**Understanding RoHS Compliant Solenoid Valves**
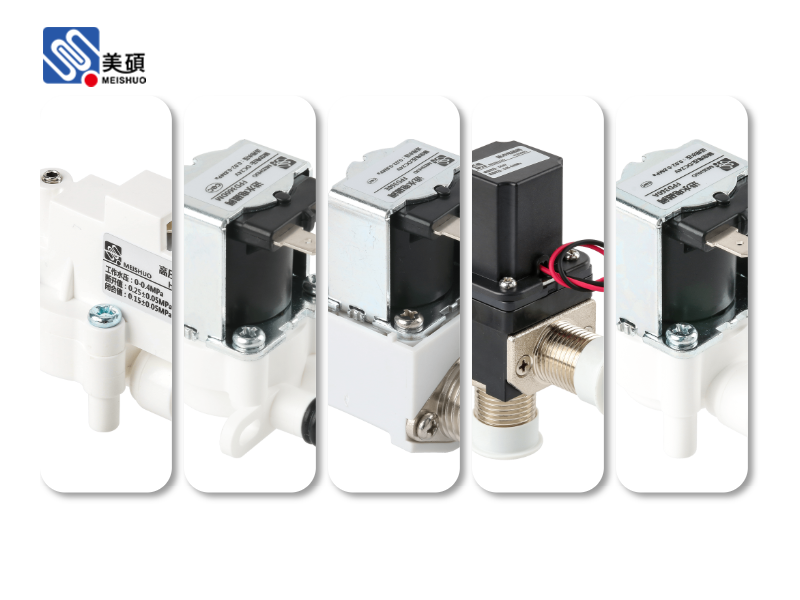
A solenoid valve is an electromechanical device that uses an electromagnet to open or close a valve. The RoHS compliant solenoid valve is specifically designed to adhere to the RoHS directive, which means it contains no hazardous substances. This not only makes it environmentally friendly but also ensures that it does not pose any health risks to the end-users.
**Benefits of RoHS Compliant Solenoid Valves**
1. **Environmental Friendliness**: By adhering to the RoHS directive, RoHS compliant solenoid valves help reduce the environmental impact of electrical and electronic equipment. This is particularly important in industries where the use of hazardous substances is prevalent.
2. **Health Safety**: The absence of hazardous substances in RoHS compliant solenoid valves ensures that they are safe for human health. This is crucial in industries where the valves are used in close proximity to people or in environments where there is a risk of exposure to harmful substances.
3. **Regulatory Compliance**: For businesses operating in the European Union or exporting to the EU, using RoHS compliant solenoid valves is mandatory. This ensures that the products meet the required standards and avoid any legal issues.
4. **Longevity and Reliability**: RoHS compliant solenoid valves are designed to be durable and reliable, ensuring long-term performance and reducing the need for frequent replacements.
**Applications of RoHS Compliant Solenoid Valves**
RoHS compliant solenoid valves find applications in a wide range of industries, including:
1. **Automotive Industry**: Used in various automotive applications, such as fuel systems, air conditioning systems, and power steering systems.
2. **Pharmaceutical Industry**: Used in pharmaceutical manufacturing processes to ensure the safety and purity of the products.
3. **Food and Beverage Industry**: Used in food processing and packaging equipment to ensure hygiene and safety.
4. **Water Treatment Industry**: Used in water treatment plants to control the flow of water and ensure its quality.
**Conclusion**
The RoHS compliant solenoid valve is a vital component in the modern world, offering numerous benefits in terms of environmental friendliness, health safety, regulatory compliance, and longevity. As industries continue to evolve and prioritize sustainability, the demand for RoHS compliant solenoid valves is expected to grow. By choosing RoHS compliant solenoid valves, businesses can not only meet the required standards but also contribute to a healthier and greener planet.
 Chat Oline