In the food and beverage industry, ensuring the highest standards of safety and hygiene is paramount. One critical component that plays a vital role in maintaining these standards is the food-grade solenoid valve. This article delves into the importance of food-grade solenoid valve certification and provides insights into the certification process and its benefits.
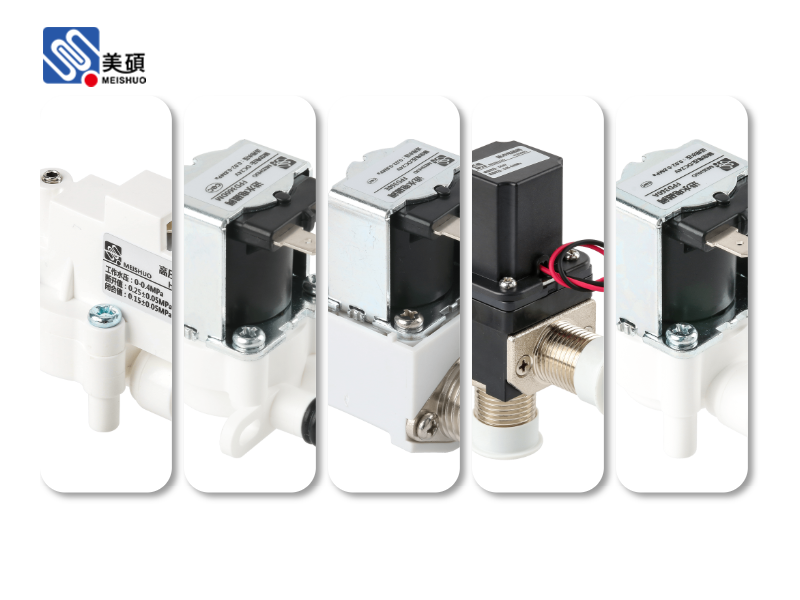
The food-grade solenoid valve is a crucial piece of equipment used in various applications within the food industry. From processing to packaging, these valves are responsible for controlling the flow of fluids, ensuring that products remain safe and uncontaminated. However, not all solenoid valves are created equal, especially when it comes to the food industry. This is where food-grade solenoid valve certification comes into play.
**Understanding Food Grade Solenoid Valve Certification**
Food-grade solenoid valve certification is a process that ensures these valves meet the strict standards required by the food industry. These standards are put in place to guarantee that the valves are made from materials that are safe for use in food applications, do not contaminate the product, and are easy to clean and maintain.
**Certification Bodies and Standards**
Several certification bodies are responsible for certifying food-grade solenoid valves. Some of the most recognized certifications include:
1. 3A Sanitary Standards: This certification is specifically designed for the food, beverage, and pharmaceutical industries. It ensures that the valves are made from materials that are safe for use in these applications. 2. NSF International: NSF is an independent organization that writes standards for food safety and water quality. Their certification for food-grade valves ensures that they meet the highest standards of safety and hygiene. 3. International Organization for Standardization (ISO): ISO 22000 is a certification that focuses on food safety management systems. It ensures that the manufacturing process of the valves adheres to strict food safety protocols.
**The Certification Process**
The certification process for food-grade solenoid valves involves several steps:
1. Material Testing: The materials used in the construction of the valve are tested to ensure they are safe for use in food applications. 2. Design and Construction Review: The design and construction of the valve are reviewed to ensure they meet the required standards. 3. Performance Testing: The valve is tested to ensure it performs as expected in various conditions, such as temperature, pressure, and fluid compatibility. 4. Cleaning and Sterilization Testing: The valve is tested to ensure it can be effectively cleaned and sterilized, which is essential in maintaining hygiene standards.
**Benefits of Food Grade Solenoid Valve Certification**
Certifying food-grade solenoid valves offers several benefits, including:
1. Enhanced Safety: By ensuring that the valves are made from safe materials and designed to meet the highest standards, certification enhances the safety of food products. 2. Improved Hygiene: Certified valves are easier to clean and maintain, which helps reduce the risk of contamination. 3. Increased Consumer Confidence: When consumers see a certification mark on a product, they are more likely to trust its safety and quality. 4. Compliance with Regulations: Certification helps companies comply with the strict regulations governing the food industry.
**Conclusion**
Food-grade solenoid valve certification is an essential process that ensures the safety, hygiene, and quality of food products. By adhering to strict standards and undergoing a thorough certification process, food-grade solenoid valves play a crucial role in maintaining the integrity of the food industry.
 Chat Oline