The food industry is a highly regulated sector that demands precision, safety, and hygiene in every aspect of production. One of the critical components that play a pivotal role in ensuring these standards is the food grade solenoid valve. This article delves into the significance of food grade solenoid valves, their working principles, and their applications in the food industry.
**Introduction**
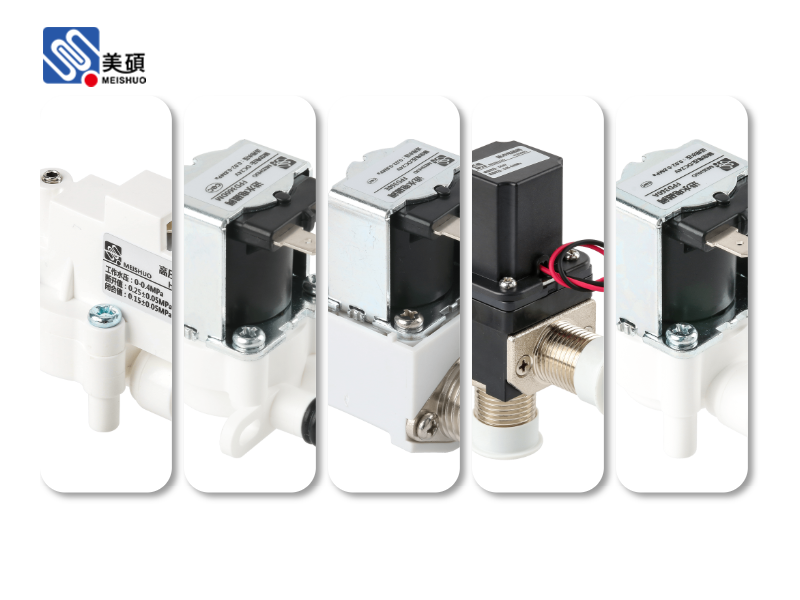
Food grade solenoid valves are specialized devices designed to control the flow of fluids in food processing systems. These valves are constructed with materials that meet stringent hygiene and safety standards, making them ideal for use in the food industry. Their primary function is to regulate the flow of liquids, gases, or slurries, ensuring that the quality and safety of food products are maintained throughout the production process.
**Understanding Food Grade Solenoid Valves**
Food grade solenoid valves are engineered to withstand the harsh conditions of the food industry. They are made from materials that are resistant to corrosion, heat, and chemicals. The following are some key features of food grade solenoid valves:
1. **Material Selection**: These valves are typically made from stainless steel, which is known for its corrosion resistance and durability. Additionally, they may include materials like polypropylene, PTFE, and EPDM, which are suitable for handling various food-grade fluids.
2. **Sealing Mechanism**: Food grade solenoid valves use high-quality seals to prevent any leakage of fluids. These seals are made from materials that are safe for food contact and can withstand repeated cleaning and sterilization processes.
3. **Design**: The design of food grade solenoid valves is simple and straightforward, which makes them easy to clean and maintain. They are also designed to minimize the risk of contamination, ensuring that the food products remain safe and uncontaminated.
**Working Principles of Food Grade Solenoid Valves**
Food grade solenoid valves operate on the principle of electromagnetic induction. When an electric current passes through the solenoid coil, it generates a magnetic field that attracts a plunger, which in turn opens or closes the valve. This process is quick and efficient, allowing for precise control of fluid flow.
**Applications in the Food Industry**
Food grade solenoid valves find extensive applications in the food industry, including:
1. **Beverage Industry**: These valves are used to control the flow of liquids, such as water, juice, and beer, in bottling and packaging processes.
2. **Dairy Industry**: Food grade solenoid valves are used to regulate the flow of milk and other dairy products during processing, packaging, and storage.
3. **Baking Industry**: These valves are used to control the flow of ingredients, such as flour, sugar, and yeast, in baking processes.
4. **Meat Processing Industry**: Food grade solenoid valves are used to control the flow of water, brine, and other fluids during the processing and packaging of meat products.
**Conclusion**
Food grade solenoid valves are indispensable components in the food industry, ensuring the safety, quality, and hygiene of food products. Their precise control over fluid flow, combined with their robust construction and material selection, makes them an ideal choice for food processing applications. As the food industry continues to evolve, the demand for high-quality, reliable food grade solenoid valves is expected to grow, further solidifying their role in the sector.
 Chat Oline