In the modern food processing industry, the efficiency and safety of operations are paramount. One critical component that plays a pivotal role in ensuring both is the food grade solenoid valve. This article delves into the significance of food grade solenoid valves, their types, applications, and the benefits they offer to the food industry.
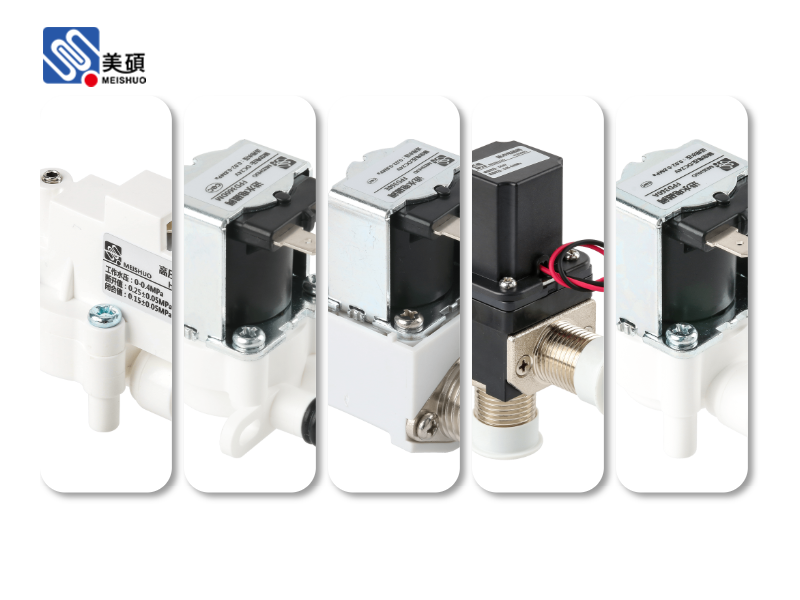
The Significance of Food Grade Solenoid Valves Food grade solenoid valves are specifically designed to handle food and beverage applications. These valves are made from materials that are non-toxic, corrosion-resistant, and easy to clean, ensuring that they meet the stringent hygiene standards required in the food processing industry. The primary function of these valves is to control the flow of liquids, gases, or slurries in a precise and reliable manner.
Types of Food Grade Solenoid Valves There are several types of food grade solenoid valves available, each designed to cater to specific application requirements. Some of the most common types include:
1. Direct Acting Solenoid Valves: These valves are suitable for low-pressure applications and are known for their simplicity and reliability.
2. Pilot Operated Solenoid Valves: These valves are ideal for high-pressure applications and can handle large flows with minimal pressure drop.
3. 3-Way Solenoid Valves: These valves are used to control the direction of flow in a system, making them versatile for various applications.
4. 4-Way Solenoid Valves: These valves can control both the direction and flow of fluid, providing greater control over the process.
Applications of Food Grade Solenoid Valves Food grade solenoid valves find applications in various stages of the food processing industry, including:
1. Packaging: Solenoid valves are used to control the flow of liquids and gases during packaging operations, ensuring the quality and safety of the final product.
2. Processing: These valves are used to control the flow of ingredients, additives, and other substances during the processing stage, maintaining consistency and hygiene.
3. Storage and Distribution: Solenoid valves are used to control the flow of liquids and gases in storage tanks and distribution systems, ensuring efficient and safe operations.
Benefits of Food Grade Solenoid Valves The use of food grade solenoid valves in the food industry offers several benefits:
1. Hygiene: These valves are designed to prevent contamination and are easy to clean, ensuring that they meet the strict hygiene standards required in the food industry.
2. Reliability: Food grade solenoid valves are known for their reliability and long lifespan, minimizing downtime and maintenance costs.
3. Precision: These valves provide precise control over the flow of fluids, ensuring consistency in the final product.
4. Energy Efficiency: Food grade solenoid valves are designed to minimize energy consumption, reducing operational costs.
Conclusion In conclusion, food grade solenoid valves are an essential component in the modern food processing industry. Their ability to control the flow of fluids in a precise and reliable manner, while meeting stringent hygiene standards, makes them an invaluable asset to the food industry. As the industry continues to evolve, the importance of these valves will only grow, ensuring the safety and efficiency of food processing operations worldwide.
 Chat Oline